How Can Ultra-Low-Speed Injection Reduce Flow Marks in Automotive Headlamp Lenses?
2026/10/09 By le zhan
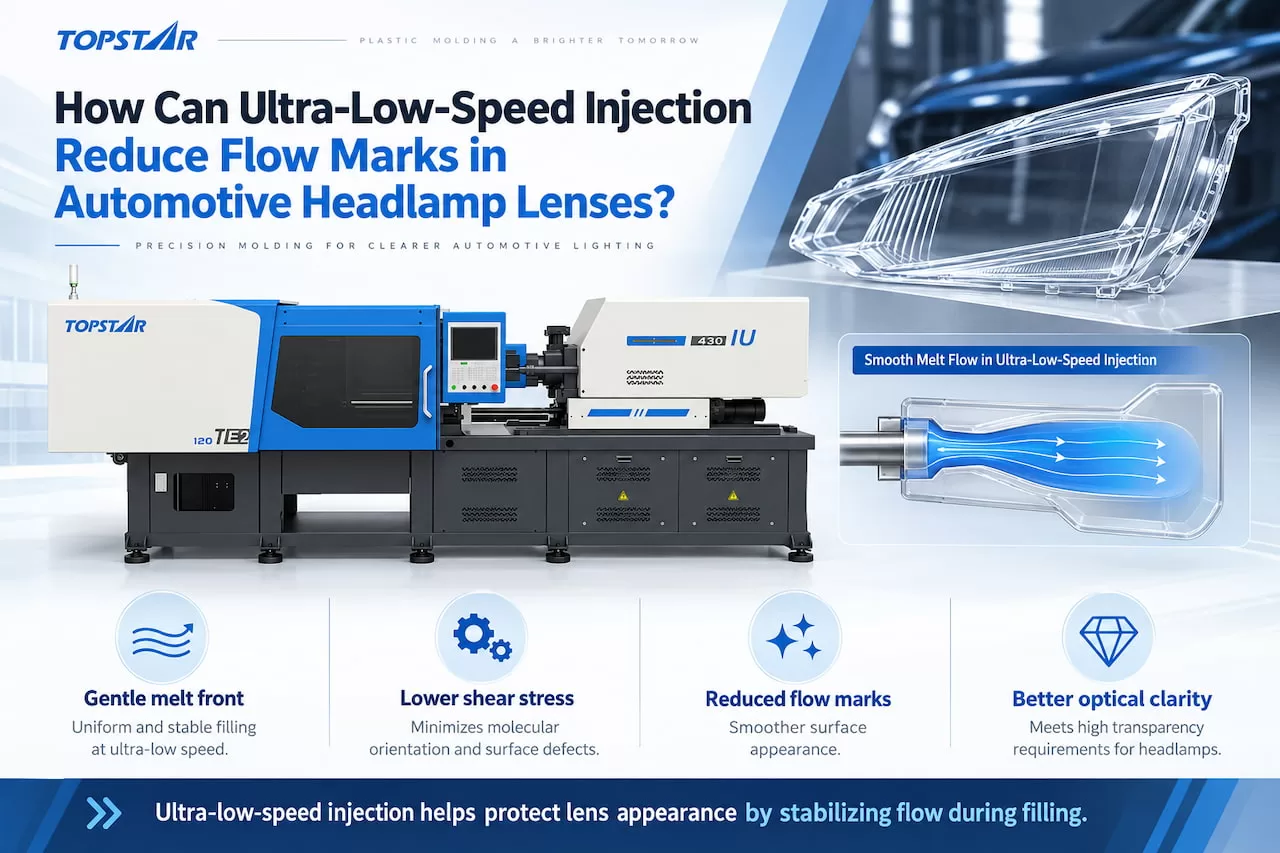
Ultra-low-speed injection molding technology can reduce flow marks on automotive headlight lenses. It works by ensuring the melt front flows smoothly through optically sensitive areas, preventing visible marks caused by sudden changes in flow velocity, shear force, and pressure. TopStar’s electric injection molding machines utilize servo direct-drive control technology combined with a high-pressure, low-speed coordinated injection process, ensuring stable melt delivery even at injection speeds as low as 0.1 mm/s. For transparent PC or PMMA optical parts, this precise control reduces flow instability while maintaining sufficient cavity pressure, improving surface-quality consistency and production yield.
Why Are Flow Marks Common in Automotive Headlight Lenses?
Automotive headlight lenses place extremely high demands on injection-molding surface quality. Materials such as PC and PMMA offer high transparency, precise optical surfaces, and excellent mold surface replication capabilities.
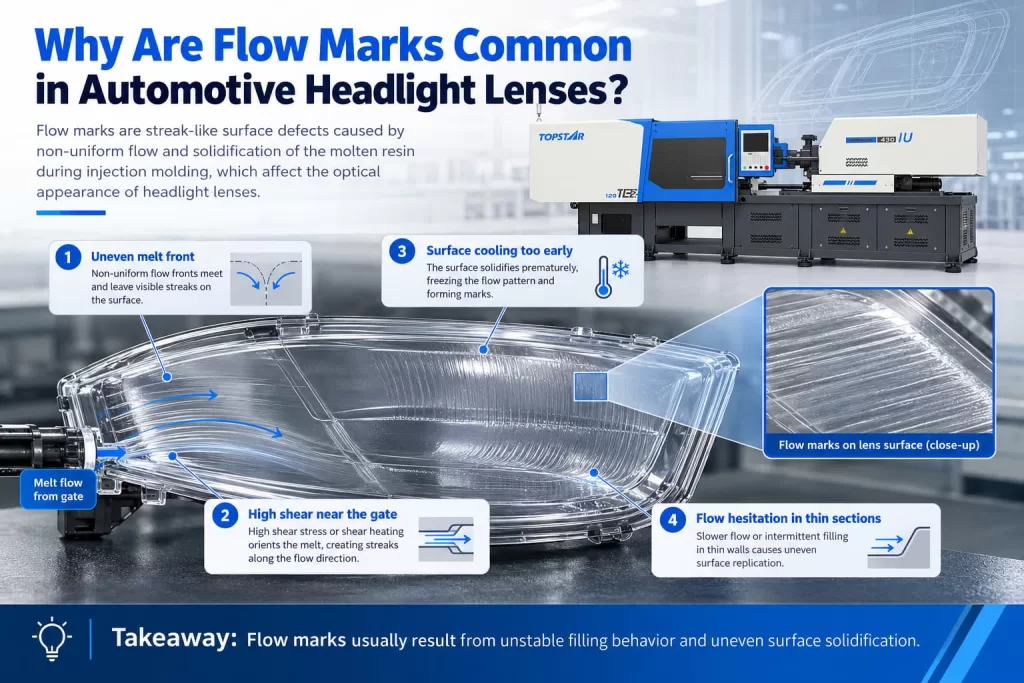
These optical properties make even minute molding defects highly visible. Subtle changes in melt front behavior may manifest after molding as differences in gloss, streaks, ripples, or flow marks. On polished headlight lenses, these defects not only affect appearance but may also compromise optical performance. Part geometry further complicates molding. Automotive lenses often feature complex designs, including long flow paths, wall thickness transitions, lettering, ribs, optical structural features, and curved surfaces. If engineers do not properly control the mold design and processing conditions, the melt may leave flow marks as it passes over lettering or other localized mold features.
Therefore, automotive headlight lenses tend to develop flow marks because the melt front moves unstably.
How Does Ultra-Low-Speed Injection Improve the Surface Quality of Automotive Lenses?
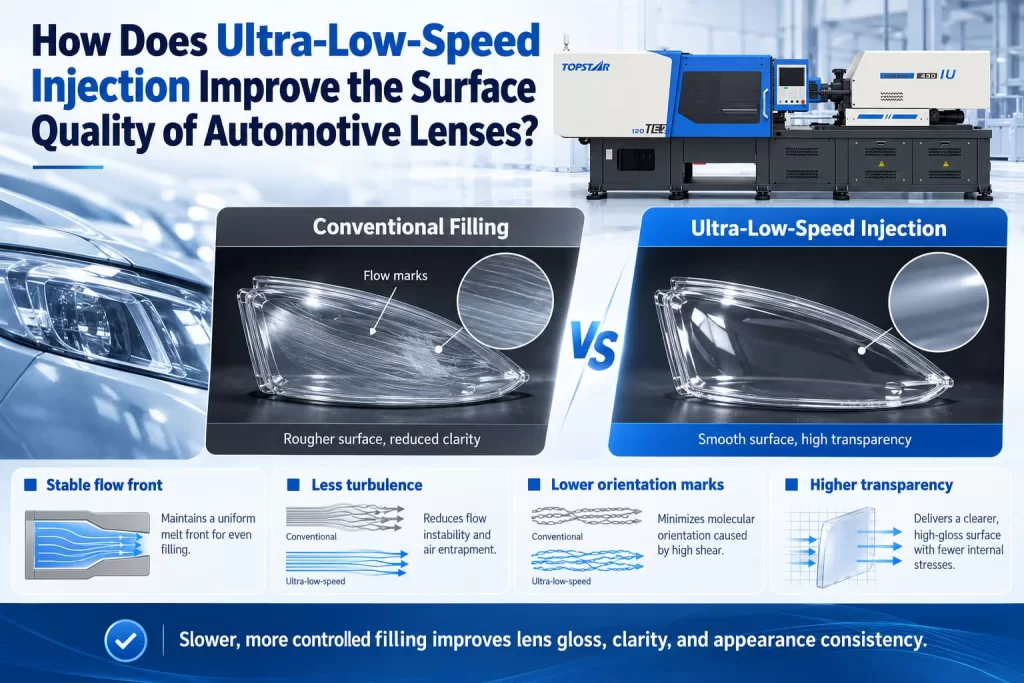
In molding optical lenses, such as automotive lenses, ultra-low-speed injection is critical when the melt must flow through sensitive areas with minimal, repeatable speed variation.
Electric injection molding machines commonly use ultra-low-speed injection because their electric servo drives can control screw movement directly, without relying on hydraulic valves or hydraulic response times. Topstar’s TEII series of electric injection molding machines utilize servo direct-drive motors that maintain smooth operation even at extremely low speeds. Their low-damping injection unit is designed for precise metering and stable melt delivery.
This matters because sudden acceleration or deceleration can change flow-front velocity, local shear rates, and pressure distribution.
The same engineering principles apply to automotive lens production:
Injection molding machines should control melt flow characteristics based on cavity geometry rather than using a single, constant speed.
Topstar’s electric injection molding platform offers ultra-low-speed precision control down to 0.1 mm/s. However, this does not mean that the entire filling process for PC or PMMA headlight lenses must be conducted at 0.1 mm/s. The 0.1 mm/s figure demonstrates the machine’s precise low-speed control capability, enabling engineers to set controlled multi-stage speed profiles that allow for slower, smoother screw movement in sensitive areas.
Ultimately, this enables:
Control of melt-front velocity as it flows through critical optical areas, preventing sudden shear or pressure changes that could cause visible defects on the finished lens surface.
How Does High Pressure Compensate for Slow Filling Speeds?
Ultra-low-speed injection molding presents a critical issue:
Because the melt flows slowly, it takes longer for heat to transfer to the mold walls. This can increase viscosity and flow resistance; if pressure is insufficient, it may also cause flow stagnation or incomplete surface replication.
Therefore, ultra-low-speed injection molding must be paired with pressure control.
A study conducted by NLM on PC optical lenses clearly demonstrates this relationship. “In this specific lens and mold configuration, injection pressures below 60 MPa result in noticeable flow marks; conversely, excessively high injection and holding pressures intensify shear forces and lead to material degradation.” The results indicate that lens molding requires a controlled pressure range and cannot rely solely on reducing the injection speed. Reference: https://pmc.ncbi.nlm.nih.gov/articles/PMC11360770/?utm_source=chatgpt.com
Topstar’s electric injection molding machines meet this requirement by coordinating high pressure with low speed. Its servo system combines position, speed, and pressure control, allowing the screw to move slowly while generating enough pressure to overcome cavity resistance and ensure continuous advancement of the melt front.
The entire process can be understood as follows:
Reduced controlled speed → Reduced sudden flow disturbances → Sufficient pressure to maintain melt flow → Stable cavity filling.
Therefore, ultra-low-speed injection molding machines require not only motors capable of low-speed movement but also precise, coordinated control of pressure and position to maintain smooth motion.
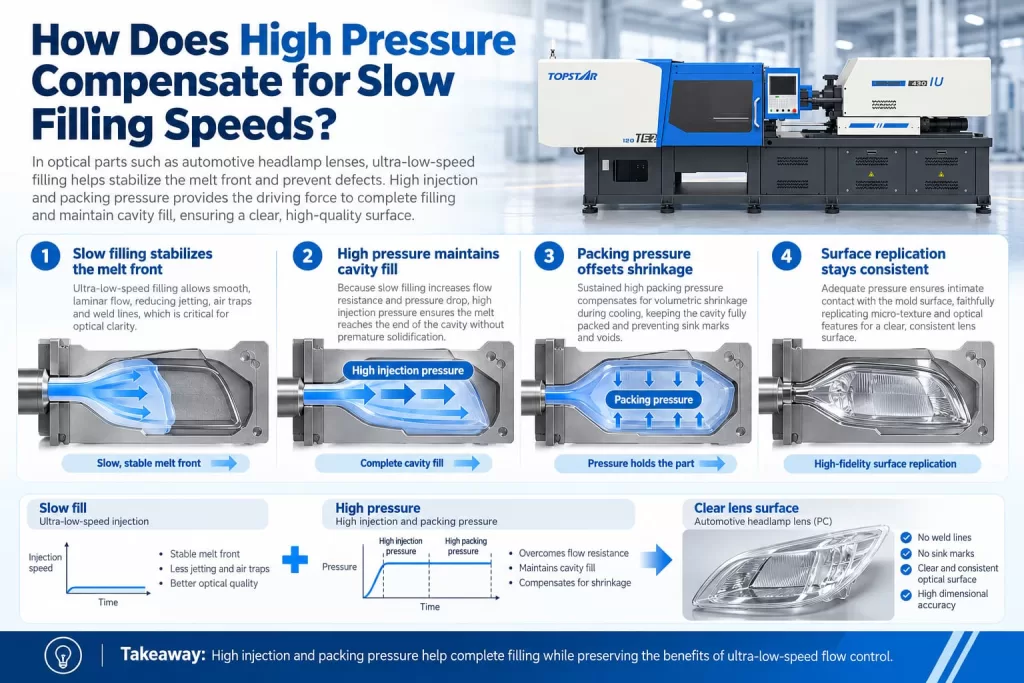
Reducing Flow Marks on Automotive Headlight Lenses Using Ultra-Low-Speed Injection Molding
Ultra-low-speed injection molding reduces flow marks on automotive headlight lenses by ensuring that the melt front flows smoothly and predictably within critical optical areas. This process uses precise, low-speed melt delivery to stabilize cavity filling, preventing visible streaks and gloss variations caused by sudden changes in speed, shear force, or pressure.
For PC and PMMA lenses, the key isn’t merely “reducing injection speed.” Instead, the injection molding machine must combine extremely low screw speeds with sufficient pressure to keep the melt advancing continuously and prevent stagnation or premature cooling. Topstar’s electric injection molding machines meet these process requirements through servo direct-drive technology, precise low-speed control down to 0.1 mm/s, and coordinated high-pressure and low-speed control functions.
The underlying mechanism can be summarized as follows:
Ultra-low-speed control → Smoother flow at the melt front → Reduced shear forces and pressure spikes → More stable cavity filling → Fewer visible flow marks.
For automotive headlight lenses, this is the core value of ultra-low-speed injection molding: it improves surface consistency by controlling melt flow within the cavity, not just by adjusting injection speed.
TRENDING POSTS
- TOPS DAY 2026: Turning Industrial AI into Real-World Impact 2026/10/09
- Breaking Through the Full Scene-to-AI Link! Topstar Industrial Data Collection Matrix Achieves Major Technical Breakthro 2026/10/09
- TOPSTAR Selected in “Forbes China AI Top 50” and Wins “2026 Embodied AI Industry Benchmark Award” 2026/10/09
- Topstar Achieves ISO 13849 Functional Safety Certification for Robotics 2026/10/09
HOT TOPIC
- .ervo motor-driven linear robots
- •
- 1.0 guangdong topstar technology co. ltd
- 1.0 topstar china
- 1.0 topstar robot
- 11
- 160℃ mold temperature controller
- 170 ton injection molding machine
- 2
- 21
- 220-ton injection molding machine
- 23
- 260 ton injection molding machine
- 3 axis robot
- 3 axis robots
- 3 in 1 Compact Dehumidifying Dryer
- 3-axis robot
- 3-axis robots
- 39
- 4 axis robot
- 4-axis SCARA robot
- 41
- 460T injection molding machine
- 5-axis CNC machine
- 62
- 90 ton injection molding machine
- accuracy
- Air Chillers
- air-cooled chillers
- all electric injection molding machine
- all electric injection molding machines
- all-electric injection molding machine
- All-electric injection molding machines
- and overall production quality. Therefore
- AP-RubberPlas
- auto cooling system
- auto loader
- Auto Loaders
- automated injection molding machine
- Automation changed engineering
- automation of injection molding robots
- automotive parts injection molding
- Auxiliary Equipment
- auxiliary machine
- Bench Injection Molding Machine
- cabinet dryer
- Cabinet dryer manufacturers
- Cabinet dryers
- cartesian coordinate robot
- Cartesian Coordinate Robots
- Cartesian injection robot
- Cartesian robot
- Central Feeding System
- Central Feeding Systems
- chiller
- CNC Drilling Machine
- CNC Drilling Machines
- cnc engraving machine manufacturer
- cnc laser cutting machine manufacturer
- CNC machine
- CNC Machine Center
- CNC Machine for Sale
- CNC Machine Manufacturing
- CNC Machine Tool
- CNC machine tool product
- CNC Machining Center
- CNC wood carving machine
- Compact Dehumidifying Dryer
- Cooling system
- Cross-Walking Single Axis Servo Cylinder Robot
- Cross-Walking Single-Axis Servo Cylinder Robot
- Cross-Walking Three-Axis/Five-Axis Servo Driven Robot
- cross-walking three-axis/five-axis servo-driven robot
- Dehumidifier Dryer
- Dehumidifying Dryer
- dehumidifying dryers
- delta parallel robot
- Desktop Injection Molding Machine
- Desktop injection molding machines
- Desktop Molding Machine
- desktop plastic injection machine
- Desktop Plastic Injection Molding Machine
- detachable autoloader
- Digital Transformation
- direct clamp injection molding machine
- Direct clamp injection molding machines
- Dosing & mixing system
- Drilling Centers
- Drying and dehumidification system
- drying and dehumidifying equipment
- Drying and Dehumidifying System
- drying system
- effective and efficient. Cabinet dryers are also used in other industries where large quantities of material need to be dried
- efficient injection molding machine
- elbow hydraulic injection molding machines
- electric injection molding machine
- electric injection molding machines
- energy-efficient injection molding robot
- energy-efficient water chiller
- energy-efficient water chillers
- energy-saving injection molding machine
- etc. Among injection molding robots
- exhibition
- features of CNC machine
- Feeding And Conveying System
- Five Axis Machine Center
- Flexible Production Line
- Fully automatic injection molding machine
- Gathering Topstar
- giant injection molding machine
- GMU-600 5-Axis Machining Center
- Granulating & Recycling System
- granulator machine
- gravimetric blender
- Heavy duty injection molding machine
- Heavy-Duty Take-Out Robot
- High-precision electric molding machines
- high-precision plastic molding machines
- high-speed all electric injection molding machine
- high-speed electric injection molding machine
- High-Speed Packaging Injection Molding
- Honeycomb rotor dehumidifier
- hopper dryer
- Hopper Dryers
- horizontal injection molding machine
- Horizontal Injection Molding Machines
- Horizontal Injection Moulding Machine
- Horizontal Mixer manufacturer
- How The CNC Machine Works
- hybrid injection molding machine
- hydraulic injection molding machine
- Hydraulic Injection Molding Machines
- in this article
- Industrial AI
- Industrial Automation
- Industrial robot
- Industrial Robot Chinese brand
- industrial robot parts
- industrial robot supplier
- Industrial robots
- Industry Chain
- Injection Manipulator
- injection manipulator robot
- injection mold machines
- Injection molding
- Injection molding automation
- Injection Molding Automation Solution
- injection molding dryer
- Injection molding equipment
- injection molding hopper dryer
- Injection molding machine
- injection molding machine brand
- Injection Molding Machine Factory
- Injection Molding Machine Manufacture
- Injection molding machine manufacturer
- injection molding machine manufacturers
- Injection molding machine procurement
- injection molding machine robotic arm
- injection molding machine with a robot
- Injection molding machines
- injection molding material dehumidifying
- injection molding plant
- injection molding process
- Injection Molding Robot
- injection molding robot arm
- Injection molding robot automation
- Injection molding robotic arm
- injection molding robots
- injection molding whole plant
- injection moulding dryer
- Injection moulding machine
- injection moulding machines
- Injection Moulding Robots
- Injection Robot
- Injection robot arm
- Injection robot manufacturer
- Injection robot wholesale
- injection robots
- Intelligent Factory
- intelligent injection molding machines
- Intelligent Manufacturing
- intelligent mold temperature
- intelligent mold temperature controller
- Intelligent mould temperature controller
- intelligent whole plant solution
- InterPlas Thailand 2025
- Introducing Injection Robot
- It is the best choice for drying large quantities of material at once. Cabinetmakers use these machines because they are fast
- Large flow water type mold temperature controller
- large injection molding machine
- large injection molding machines
- Learn what industrial automation and robotics is
- linear robot
- linear robots
- low speed sound-proof granulator
- machine plastic molding
- make sure to add some! Improvements (2) Keyphrase in introduction: Your keyphrase or its synonyms appear in the first paragraph of the copy
- manipulator machine
- manufacturing
- Manufacturing Innovation
- medical grade injection molding machines
- Medical Injection Molding
- medical injection molding machine
- medical injection molding machines
- micro injection molding machine
- middle speed granulator
- Mini CNC machine manufacturers.
- mobile cover making machine
- Mold Temperature Control System
- mold temperature controller
- mold temperature controllers
- molding machine
- molding material Dehumidifying System
- mould temperature control system
- mould temperature controller
- mould temperature controller
- mould temperature controllers
- New electric injection molding machine
- Nitrogen Dryer
- nitrogen dryer manufacturer
- nitrogen dryer system manufacturer
- Oil type mold temperature controller
- Oil type mold temperature controllers
- open day
- optical component injection molding
- Optical-grade dehumidifying dryer
- Outbound links: No outbound links appear in this page. Add some! Images: No images appear on this page. Add some! Internal links: No internal links appear in this page
- packaging injection molding
- Packaging Solutions
- PET Preform injection molding
- phone case maker machine
- phone case making machine
- phone cover making machine
- PID Control Mold Temperature Controller
- plastic auto loader
- plastic bottle making machine
- plastic bottle manufacturing
- plastic bucket making machine
- plastic bucket manufacturing
- Plastic chair making machine
- plastic dryer for injection molding
- plastic forming equipment
- Plastic Granulator
- Plastic Granulators
- plastic hopper dryer
- plastic injection machine
- plastic injection machines
- plastic injection molding
- Plastic injection molding equipment
- Plastic injection molding machine
- Plastic Injection Molding Machines
- plastic injection moulding machine
- plastic injection moulding machines
- plastic injection robot
- plastic molding
- Plastic Molding Industry
- Plastic Molding machine
- plastic molding machine 1
- Plastic Molding Machines
- plastic molding press
- plastic moulding machine
- plastic phone case making machine
- plastic-molding machine
- powerful granulator
- Powerful Type Sound-Proof Granulator
- precision injection molding
- precision injection molding machines
- production of plastic seats
- pure water mould temperature controller
- Robot injection molding
- robot injection molding machine
- robot manufacturing companies
- Robotic arm for injection molding machine
- robotic injection molding machines
- robotics in injection molding
- SCARA robot
- SCARA robots
- Screw dosers
- Service-oriented manufacturing
- Servo Cylinder Robot
- servo driven robot
- Servo Driven Robots
- servo injection molding machine
- servo injection robots
- servo motor-driven linear robots
- servo-driven 3-axis robot
- Servo-driven injection molding machine
- Servo-Driven Robot
- Setup of injection machine
- Silicone Injection Molding Machine
- six-axis industrial robot
- Smart Manufacturing
- soundproof granulator
- Sprue Picker
- Stainless Hopper Dryer
- Stainless Hopper Dryers
- star club
- swing arm robot
- T1 Cartesian injection robot
- take-out robot
- take-out robots
- Thailand 4.0
- the choice between servo-driven robots and hydraulic robots will have a certain impact on efficiency
- the most popular injection molding machine
- the type of injection molding robot
- TIC2000 Control System
- TMII injection molding machine
- toggle clamp injection molding machine
- Toggle Hydraulic Injection Molding Machines
- toggle injection molding machine
- Top 10 brands of injection robots
- Topstar
- Topstar Electric Injection Molding Machine InterPlas Thailand 2025 Smart Manufacturing Thailand 4.0
- Topstar Engineering
- Topstar Industrial Robots
- Topstar injection molding intelligent
- Topstar Scara Robots
- Useful Injection molding machine
- Vertical machining centers
- volumetric type blender
- Washing Machine Case Molding Solution
- water chiller
- water chillers
- water distributor
- water type mold temperature controller
- Water Type MoldTemperature Controller
- Water-Cooled Chillers
- Water-cooled Mold Temperature Controller
- water-type mold temperature controller
- Water-Type Mould Temperature Controllers
- We often face choices when performing injection molding. We will choose the type of injection molding machine
- wholesale of injection molding machines
- x carve CNC
- 热门查询 点击次数 展示 排名 topstar