How Should Injection Speed and Pressure Be Balanced During Precision Injection Molding?
2026/10/12 By le zhan
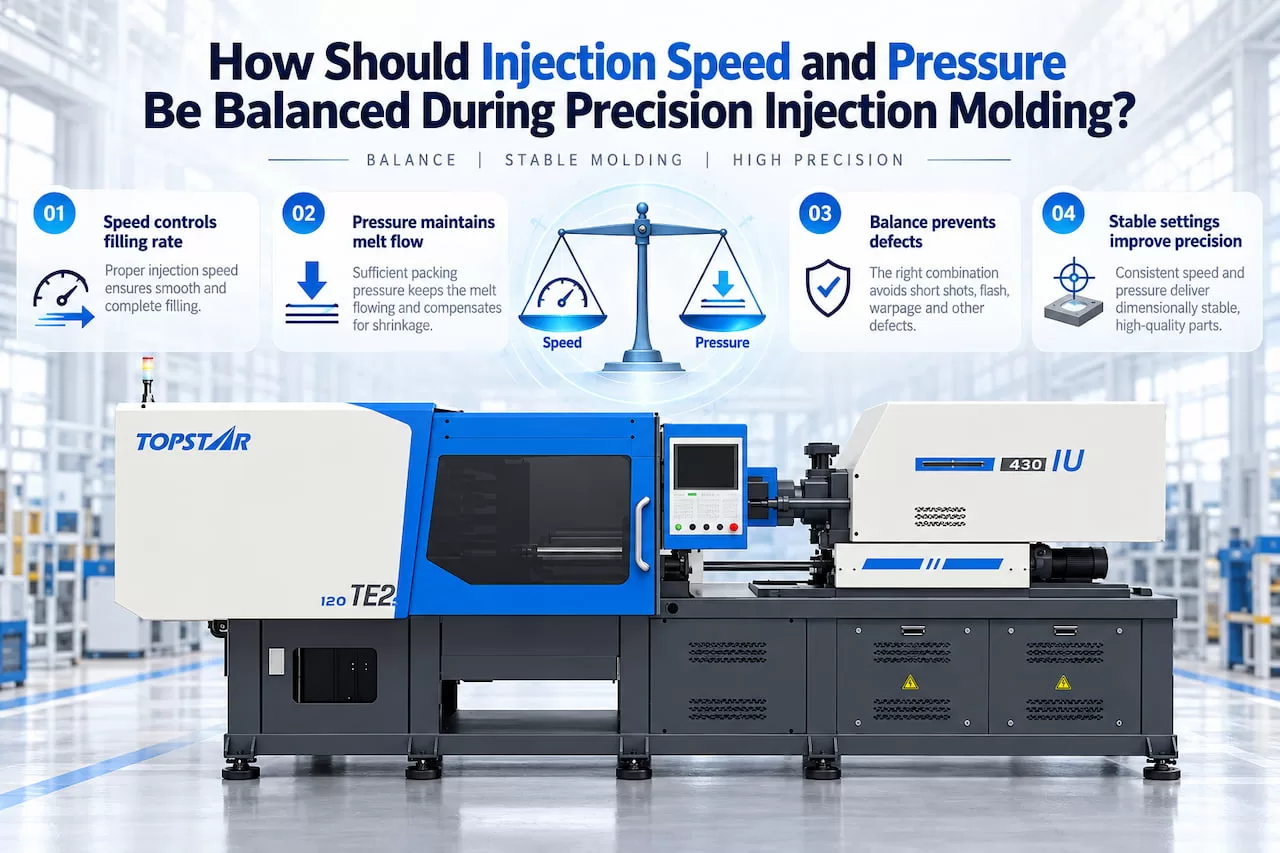
In injection molding, the injection speed is primarily used to control the cavity filling process. In contrast, injection pressure must provide enough force to maintain the preset flow conditions without exceeding the limit. For precision injection molding operations, we typically recommend that customers first set a stable speed curve and set the pressure upper limit high enough to avoid restricting speed control; Subsequently, as the filling process nears completion, the control switches from speed control to holding pressure control. The purpose of this approach is not to achieve the highest speed or maximum pressure, but to obtain repeatable melt front flow rates and cavity pressure curves, thereby ensuring the part is filled without causing flash, excessive shear, scorch marks, or over-holding pressure.
What Roles Do Injection Speed and Pressure Play in Precision Injection Molding?
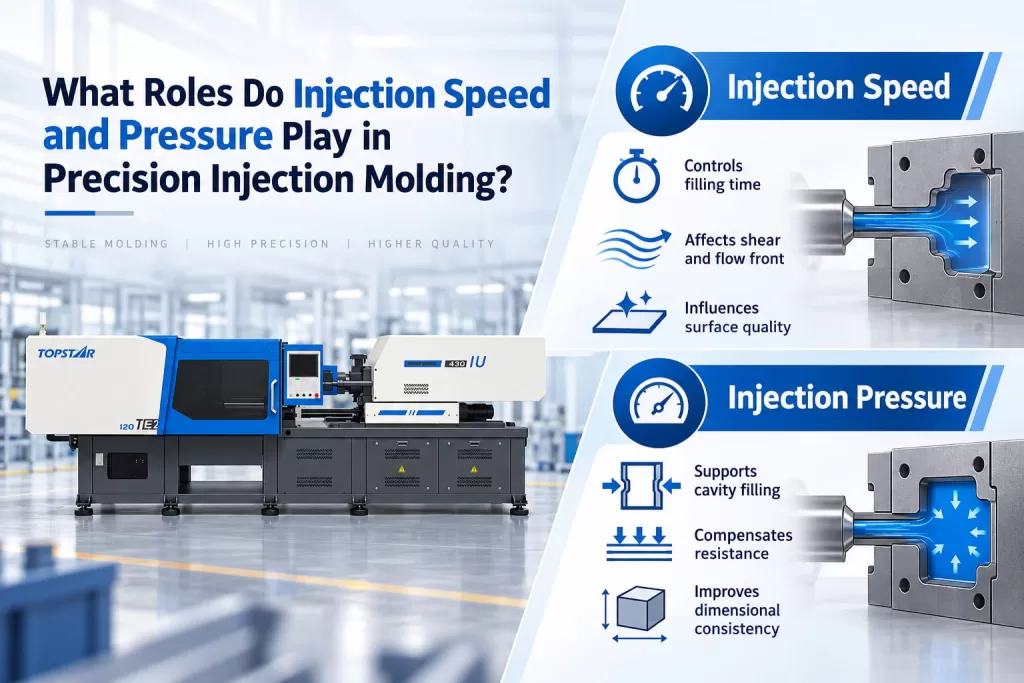
The first step in balancing injection speed and injection pressure is to understand that they serve different functions.
During the main filling phase, the injection molding machine typically controls the screw speed. Injection speed determines the melt front flow rate through the runner, gate, and cavity. This directly affects shear rate, cooling during filling, surface appearance, weld-line formation, and required pressure.
Pressure, on the other hand, is the force required to overcome resistance as the melt flows through the runner. In speed-controlled mode, the injection molding machine generates sufficient pressure to maintain the set screw speed until a preset pressure limit is reached. Generally, operators should not attempt to control the filling process by increasing pressure first.
Simply put:
Injection speed controls melt flow.
Injection pressure provides the force required to achieve that flow.
For this reason, even with the same injection speed, two different molds may require vastly different pressures. If the part has thin walls, a small gate, a long flow path, a low melt temperature, or high material viscosity, greater flow resistance will result, requiring higher pressure to maintain the same flow rate.
What Happens If the Speed and Pressure Are Too High?
Increasing both parameters simultaneously does not necessarily improve filling results.
Excessively high injection speed generates high shear stress and shear heat. If the machine injects material at high speed and maintains excessive pressure during the final stage of filling, cavity pressure can rise sharply. This can lead to the following consequences:
- Flash (burrs) forming at the parting line;
- Excessive internal stress;
- Difficulty in demolding;
- Burn marks near trapped air pockets;
- Excessive holding pressure and dimensional deviations;
- Unnecessary stress on the mold and clamping mechanism.
Therefore, the right approach is to maintain adequate speed while keeping pressure under control, rather than simply increasing set values.
In precision injection molding, should injection speed or pressure be adjusted first?
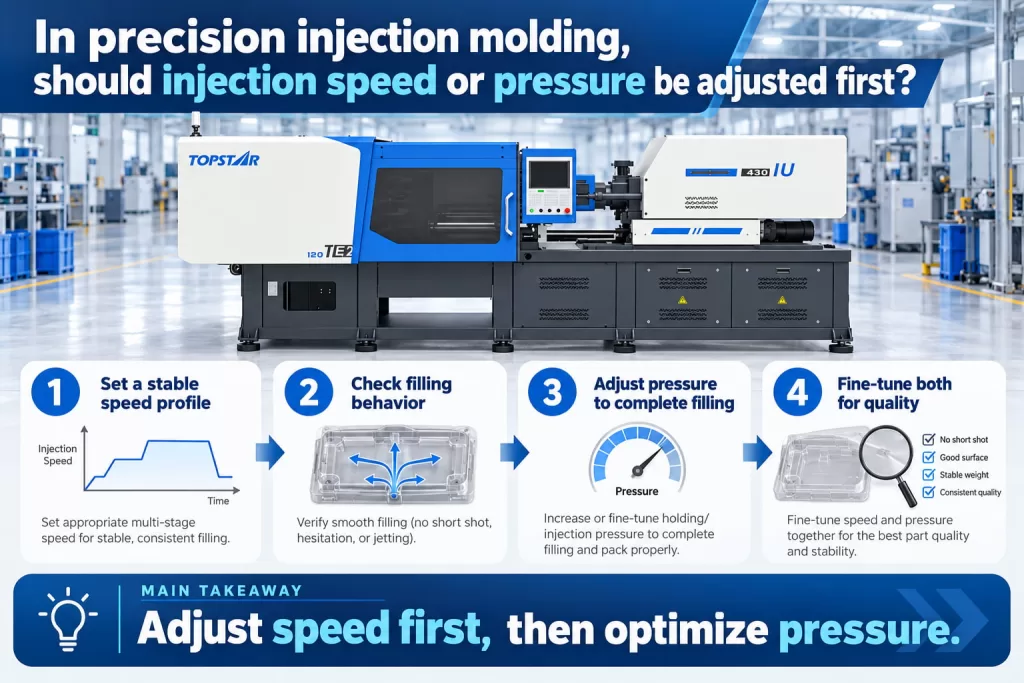
For most precision injection molding applications, set the injection speed profile first.
Use the processing parameter ranges provided by the resin supplier, along with the mold geometry, wall thickness, gate size, and expected fill time, to set these parameters. Adjust the screw speed until the cavity fills smoothly and repeatedly, with no stalling, jetting, excessive shear, or premature solidification. Then, monitor the actual injection pressure.
If the injection molding machine reaches the pressure limit before achieving the preset speed, the process is in a “pressure-limited” state. In this case, increasing the speed setting further won’t accelerate melt flow because the machine has already reached the maximum allowable pressure.
At this point, engineers should analyze the causes of excessive pressure requirements. Common causes include:
Too small a gate → Too thin wall thickness → Low melt temperature → Low mold temperature → Obstructed runner → High resin viscosity.
If the mold and material perform as expected, operators can increase the pressure limit as long as the injection molding machine, mould, and clamping system remain within their safe operating limits. However, if the pressure demand is already too high, simply raising the limit may mask defects in the process or mold design.
The recommended adjustment logic is as follows:
Set a stable speed curve → Verify actual pressure requirements → Confirm sufficient pressure margin → Optimize the V/P transition → Adjust the holding pressure.
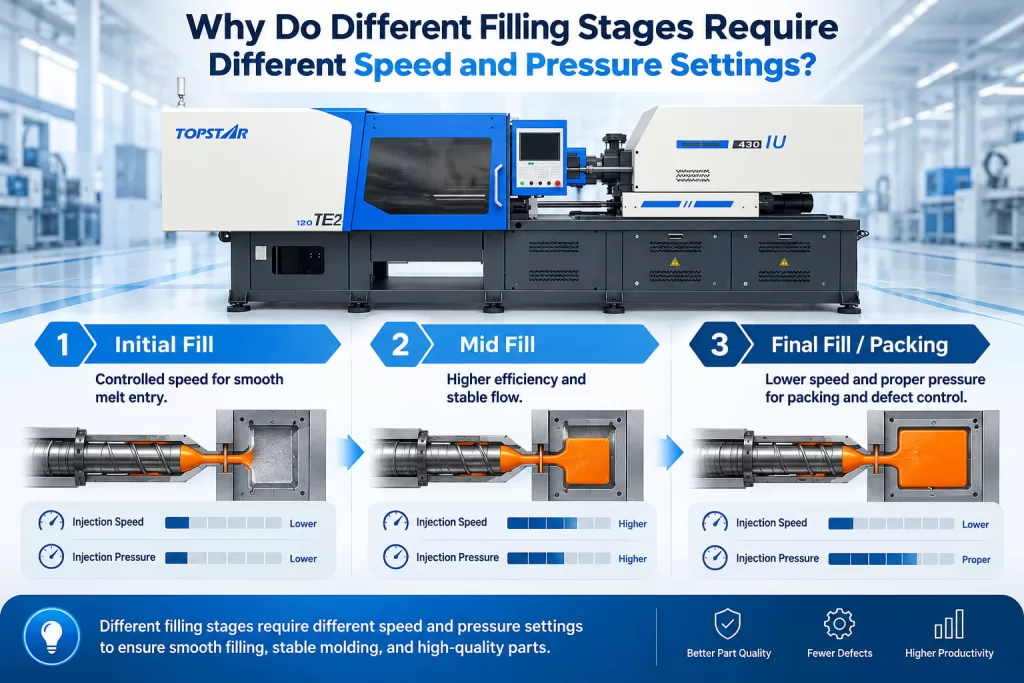
Why Do Different Filling Stages Require Different Speed and Pressure Settings?
A single injection speed is often insufficient to meet the filling requirements of the entire cavity. Flow conditions at the beginning, middle, and end of the filling process often differ significantly.
During the initial injection phase, the melt must flow through the nozzle, runner, and gate. Excessively high initial acceleration can cause jet formation or flow instability; therefore, for certain molds, a controlled initial speed is preferable. During the main phase of cavity filling, you can typically increase the filling speed to maintain a stable melt-front advance, preventing viscosity increases caused by excessive cooling.
As the cavity nears full filling, you usually need to reduce speed or switch to pressure-controlled mode. Maintaining high injection speeds during the final stage of filling can cause a sudden pressure surge because very little cavity space remains for the melt.
This is precisely the purpose of the V/P switch: transitioning from speed-controlled filling to pressure-controlled holding.
This phased process strategy is particularly useful for molding precision parts with varying wall thicknesses, multiple gates, optical surfaces, fine features, or strict dimensional tolerance requirements.
Practical Methods for Balancing Injection Speed and Pressure in Precision Injection Molding
From a Topstar engineering perspective, the first step is to ensure stable material dryness, melt temperature, mold temperature, and shot volume. If the material or thermal conditions are unstable, adjusting speed and pressure alone will not provide reliable compensation.
Second, establish a filling curve. By observing short-shot conditions, part weight, screw position, filling time, cavity pressure (if applicable), and surface quality, confirm that the melt front advances consistently.
Next, evaluate the pressure requirements. The upper limit of injection pressure should be set to ensure the machine can operate according to the preset speed curve while maintaining a sufficient safety margin.
Then, optimize the speed/pressure (V/P) transition. Transitioning too early may result in short shots or require excessive holding pressure to complete filling; transitioning too late may cause flash and pressure spikes.
Finally, adjust the holding pressure and holding time separately. Holding pressure compensates for material shrinkage after filling, not unstable speed control during the filling phase.
This balance can be summarized as follows:
Injection speed determines the flow behavior of the melt front → Injection pressure provides the force required to maintain that speed → V/P switching prevents pressure spikes at the end of filling → Holding pressure stabilizes the final dimensions of the part.
We recommend this method for balancing injection speed and pressure in precision injection molding. The optimal process isn’t the setting with the highest numerical values on the controller; it’s the one that ensures stable speed during filling, keeps pressure within a controlled operating range, and maintains consistent switching between cycles.
TRENDING POSTS
- TOPS DAY 2026: Turning Industrial AI into Real-World Impact 2026/10/12
- Breaking Through the Full Scene-to-AI Link! Topstar Industrial Data Collection Matrix Achieves Major Technical Breakthro 2026/10/12
- TOPSTAR Selected in “Forbes China AI Top 50” and Wins “2026 Embodied AI Industry Benchmark Award” 2026/10/12
- Topstar Achieves ISO 13849 Functional Safety Certification for Robotics 2026/10/12
HOT TOPIC
- .ervo motor-driven linear robots
- •
- 1.0 guangdong topstar technology co. ltd
- 1.0 topstar china
- 1.0 topstar robot
- 11
- 160℃ mold temperature controller
- 170 ton injection molding machine
- 2
- 21
- 220-ton injection molding machine
- 23
- 260 ton injection molding machine
- 3 axis robot
- 3 axis robots
- 3 in 1 Compact Dehumidifying Dryer
- 3-axis robot
- 3-axis robots
- 39
- 4 axis robot
- 4-axis SCARA robot
- 41
- 460T injection molding machine
- 5-axis CNC machine
- 62
- 90 ton injection molding machine
- accuracy
- Air Chillers
- air-cooled chillers
- all electric injection molding machine
- all electric injection molding machines
- all-electric injection molding machine
- All-electric injection molding machines
- and overall production quality. Therefore
- AP-RubberPlas
- auto cooling system
- auto loader
- Auto Loaders
- automated injection molding machine
- Automation changed engineering
- automation of injection molding robots
- automotive parts injection molding
- Auxiliary Equipment
- auxiliary machine
- Bench Injection Molding Machine
- cabinet dryer
- Cabinet dryer manufacturers
- Cabinet dryers
- cartesian coordinate robot
- Cartesian Coordinate Robots
- Cartesian injection robot
- Cartesian robot
- Central Feeding System
- Central Feeding Systems
- chiller
- CNC Drilling Machine
- CNC Drilling Machines
- cnc engraving machine manufacturer
- cnc laser cutting machine manufacturer
- CNC machine
- CNC Machine Center
- CNC Machine for Sale
- CNC Machine Manufacturing
- CNC Machine Tool
- CNC machine tool product
- CNC Machining Center
- CNC wood carving machine
- Compact Dehumidifying Dryer
- Cooling system
- Cross-Walking Single Axis Servo Cylinder Robot
- Cross-Walking Single-Axis Servo Cylinder Robot
- Cross-Walking Three-Axis/Five-Axis Servo Driven Robot
- cross-walking three-axis/five-axis servo-driven robot
- Dehumidifier Dryer
- Dehumidifying Dryer
- dehumidifying dryers
- delta parallel robot
- Desktop Injection Molding Machine
- Desktop injection molding machines
- Desktop Molding Machine
- desktop plastic injection machine
- Desktop Plastic Injection Molding Machine
- detachable autoloader
- Digital Transformation
- direct clamp injection molding machine
- Direct clamp injection molding machines
- Dosing & mixing system
- Drilling Centers
- Drying and dehumidification system
- drying and dehumidifying equipment
- Drying and Dehumidifying System
- drying system
- effective and efficient. Cabinet dryers are also used in other industries where large quantities of material need to be dried
- efficient injection molding machine
- elbow hydraulic injection molding machines
- electric injection molding machine
- electric injection molding machines
- energy-efficient injection molding robot
- energy-efficient water chiller
- energy-efficient water chillers
- energy-saving injection molding machine
- etc. Among injection molding robots
- exhibition
- features of CNC machine
- Feeding And Conveying System
- Five Axis Machine Center
- Flexible Production Line
- Fully automatic injection molding machine
- Gathering Topstar
- giant injection molding machine
- GMU-600 5-Axis Machining Center
- Granulating & Recycling System
- granulator machine
- gravimetric blender
- Heavy duty injection molding machine
- Heavy-Duty Take-Out Robot
- High-precision electric molding machines
- high-precision plastic molding machines
- high-speed all electric injection molding machine
- high-speed electric injection molding machine
- High-Speed Packaging Injection Molding
- Honeycomb rotor dehumidifier
- hopper dryer
- Hopper Dryers
- horizontal injection molding machine
- Horizontal Injection Molding Machines
- Horizontal Injection Moulding Machine
- Horizontal Mixer manufacturer
- How The CNC Machine Works
- hybrid injection molding machine
- hydraulic injection molding machine
- Hydraulic Injection Molding Machines
- in this article
- Industrial AI
- Industrial Automation
- Industrial robot
- Industrial Robot Chinese brand
- industrial robot parts
- industrial robot supplier
- Industrial robots
- Industry Chain
- Injection Manipulator
- injection manipulator robot
- injection mold machines
- Injection molding
- Injection molding automation
- Injection Molding Automation Solution
- injection molding dryer
- Injection molding equipment
- injection molding hopper dryer
- Injection molding machine
- injection molding machine brand
- Injection Molding Machine Factory
- Injection Molding Machine Manufacture
- Injection molding machine manufacturer
- injection molding machine manufacturers
- Injection molding machine procurement
- injection molding machine robotic arm
- injection molding machine with a robot
- Injection molding machines
- injection molding material dehumidifying
- injection molding plant
- injection molding process
- Injection Molding Robot
- injection molding robot arm
- Injection molding robot automation
- Injection molding robotic arm
- injection molding robots
- injection molding whole plant
- injection moulding dryer
- Injection moulding machine
- injection moulding machines
- Injection Moulding Robots
- Injection Robot
- Injection robot arm
- Injection robot manufacturer
- Injection robot wholesale
- injection robots
- Intelligent Factory
- intelligent injection molding machines
- Intelligent Manufacturing
- intelligent mold temperature
- intelligent mold temperature controller
- Intelligent mould temperature controller
- intelligent whole plant solution
- InterPlas Thailand 2025
- Introducing Injection Robot
- It is the best choice for drying large quantities of material at once. Cabinetmakers use these machines because they are fast
- Large flow water type mold temperature controller
- large injection molding machine
- large injection molding machines
- Learn what industrial automation and robotics is
- linear robot
- linear robots
- low speed sound-proof granulator
- machine plastic molding
- make sure to add some! Improvements (2) Keyphrase in introduction: Your keyphrase or its synonyms appear in the first paragraph of the copy
- manipulator machine
- manufacturing
- Manufacturing Innovation
- medical grade injection molding machines
- Medical Injection Molding
- medical injection molding machine
- medical injection molding machines
- micro injection molding machine
- middle speed granulator
- Mini CNC machine manufacturers.
- mobile cover making machine
- Mold Temperature Control System
- mold temperature controller
- mold temperature controllers
- molding machine
- molding material Dehumidifying System
- mould temperature control system
- mould temperature controller
- mould temperature controller
- mould temperature controllers
- New electric injection molding machine
- Nitrogen Dryer
- nitrogen dryer manufacturer
- nitrogen dryer system manufacturer
- Oil type mold temperature controller
- Oil type mold temperature controllers
- open day
- optical component injection molding
- Optical-grade dehumidifying dryer
- Outbound links: No outbound links appear in this page. Add some! Images: No images appear on this page. Add some! Internal links: No internal links appear in this page
- packaging injection molding
- Packaging Solutions
- PET Preform injection molding
- phone case maker machine
- phone case making machine
- phone cover making machine
- PID Control Mold Temperature Controller
- plastic auto loader
- plastic bottle making machine
- plastic bottle manufacturing
- plastic bucket making machine
- plastic bucket manufacturing
- Plastic chair making machine
- plastic dryer for injection molding
- plastic forming equipment
- Plastic Granulator
- Plastic Granulators
- plastic hopper dryer
- plastic injection machine
- plastic injection machines
- plastic injection molding
- Plastic injection molding equipment
- Plastic injection molding machine
- Plastic Injection Molding Machines
- plastic injection moulding machine
- plastic injection moulding machines
- plastic injection robot
- plastic molding
- Plastic Molding Industry
- Plastic Molding machine
- plastic molding machine 1
- Plastic Molding Machines
- plastic molding press
- plastic moulding machine
- plastic phone case making machine
- plastic-molding machine
- powerful granulator
- Powerful Type Sound-Proof Granulator
- precision injection molding
- precision injection molding machines
- production of plastic seats
- pure water mould temperature controller
- Robot injection molding
- robot injection molding machine
- robot manufacturing companies
- Robotic arm for injection molding machine
- robotic injection molding machines
- robotics in injection molding
- SCARA robot
- SCARA robots
- Screw dosers
- Service-oriented manufacturing
- Servo Cylinder Robot
- servo driven robot
- Servo Driven Robots
- servo injection molding machine
- servo injection robots
- servo motor-driven linear robots
- servo-driven 3-axis robot
- Servo-driven injection molding machine
- Servo-Driven Robot
- Setup of injection machine
- Silicone Injection Molding Machine
- six-axis industrial robot
- Smart Manufacturing
- soundproof granulator
- Sprue Picker
- Stainless Hopper Dryer
- Stainless Hopper Dryers
- star club
- swing arm robot
- T1 Cartesian injection robot
- take-out robot
- take-out robots
- Thailand 4.0
- the choice between servo-driven robots and hydraulic robots will have a certain impact on efficiency
- the most popular injection molding machine
- the type of injection molding robot
- TIC2000 Control System
- TMII injection molding machine
- toggle clamp injection molding machine
- Toggle Hydraulic Injection Molding Machines
- toggle injection molding machine
- Top 10 brands of injection robots
- Topstar
- Topstar Electric Injection Molding Machine InterPlas Thailand 2025 Smart Manufacturing Thailand 4.0
- Topstar Engineering
- Topstar Industrial Robots
- Topstar injection molding intelligent
- Topstar Scara Robots
- Useful Injection molding machine
- Vertical machining centers
- volumetric type blender
- Washing Machine Case Molding Solution
- water chiller
- water chillers
- water distributor
- water type mold temperature controller
- Water Type MoldTemperature Controller
- Water-Cooled Chillers
- Water-cooled Mold Temperature Controller
- water-type mold temperature controller
- Water-Type Mould Temperature Controllers
- We often face choices when performing injection molding. We will choose the type of injection molding machine
- wholesale of injection molding machines
- x carve CNC
- 热门查询 点击次数 展示 排名 topstar