How Does a High-Speed Injection Molding Machine Reduce Thin-Wall Food Container Cycles?
2026/09/23 By le zhan
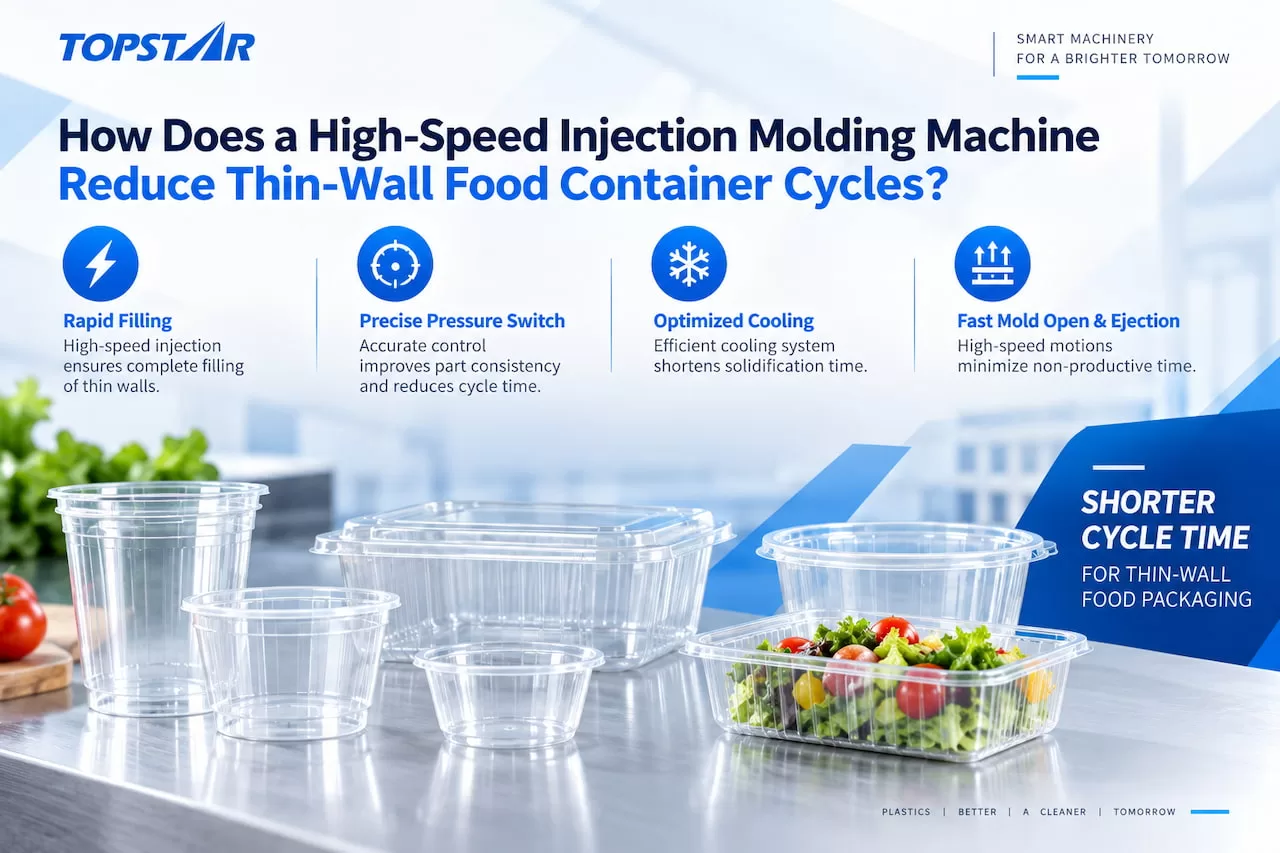
High-speed injection molding machine reduce molding cycle time for thin-walled food containers by shortening fill time, accelerating mold movement and part ejection, and cooling parts only as long as needed to prevent deformation. However, for thin-walled packaging, speed alone is not enough. The injection molding machine must fill the cavity before the melt front solidifies, maintain repeatable pressure and position control, and coordinate cooling, ejection, and automation actions without increasing idle time. Therefore, the actual goal is not the highest injection speed, but rather the shortest and most stable molding cycle while ensuring smooth edges, uniform wall thickness, and reliable stacking.
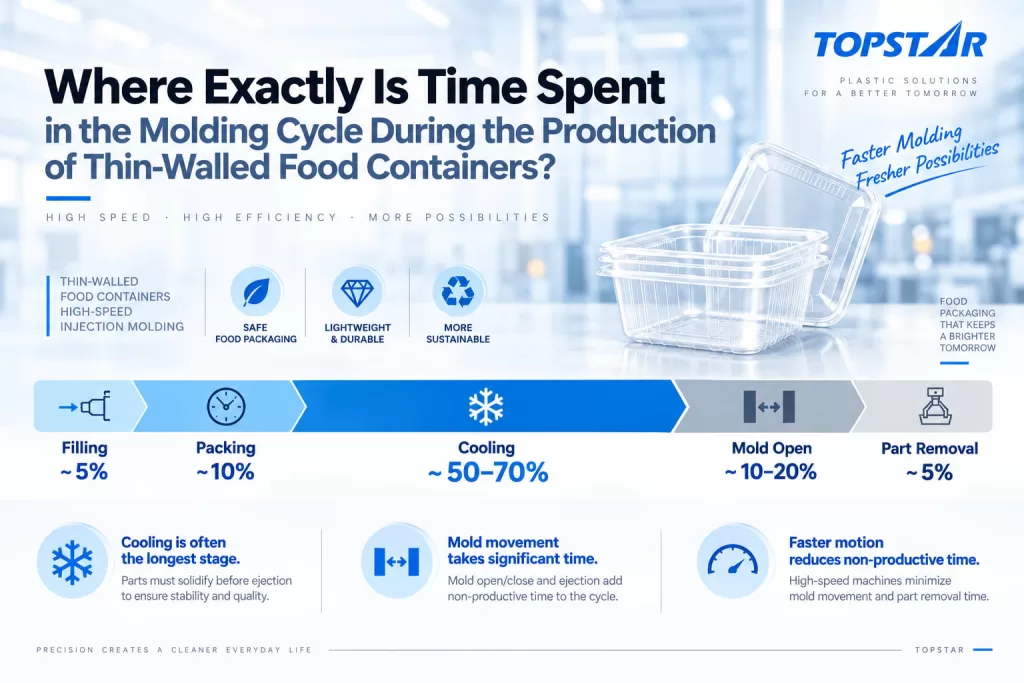
Where Exactly Is Time Spent in the Molding Cycle During the Production of Thin-Walled Food Containers?
When manufacturers produce thin-walled food containers, they often assume injection takes the most time because the machine must fill the cavity with plastic at extremely high speeds. However, in practice, the full molding cycle includes injection, holding pressure, cooling, mold opening, part removal, and mold closing. As injection speed increases, the time spent on other stages in the total cycle increases accordingly.
A real-world case study on high-speed thin-wall container production clearly illustrates this point: “In a four-cavity food packaging production process with a total cycle time of 3.15 seconds, injection took only 0.08 seconds, while cooling took 0.8 seconds, and demolding (including part removal) took 2.27 seconds. Of the demolding time, 1.27 seconds were spent on mold movement, and 1.0 second on the robot retrieving the product.”
This indicates that a high-speed injection molding machine must optimize the entire molding cycle, not just maximize injection speed.
What should the filling speed be set to for a high-speed injection molding machine?
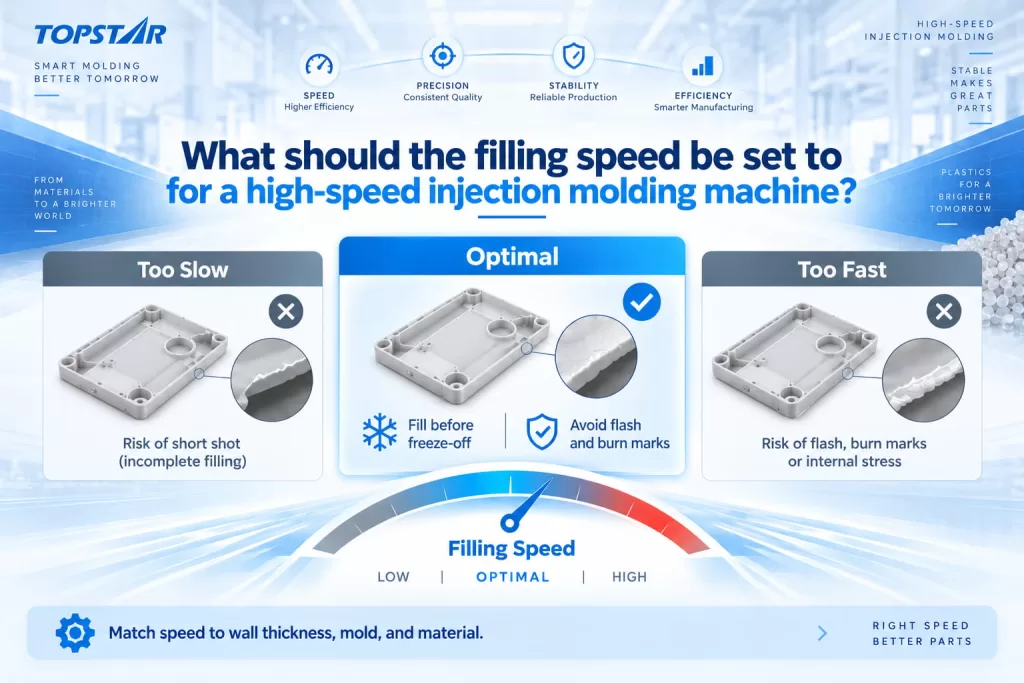
No single universal injection speed applies to all thin-walled food containers. The appropriate injection speed depends on wall thickness, flow length, gate design, resin grade, melt temperature, mold temperature, and cavity balance. Our goal is to fill the cavity before the melt front solidifies, while avoiding unnecessary shear heating, jet flow, or pressure spikes.
We recommend a practical approach to process setup: First, refer to the processing parameter ranges recommended by the mold and resin suppliers. Use short-shot tests or filling simulations to determine the required filling time. Then increase the injection speed only as much as needed to achieve complete, stable filling. The goal is to find the fastest, most repeatable filling curve, not simply chase the highest value displayed on the controller.
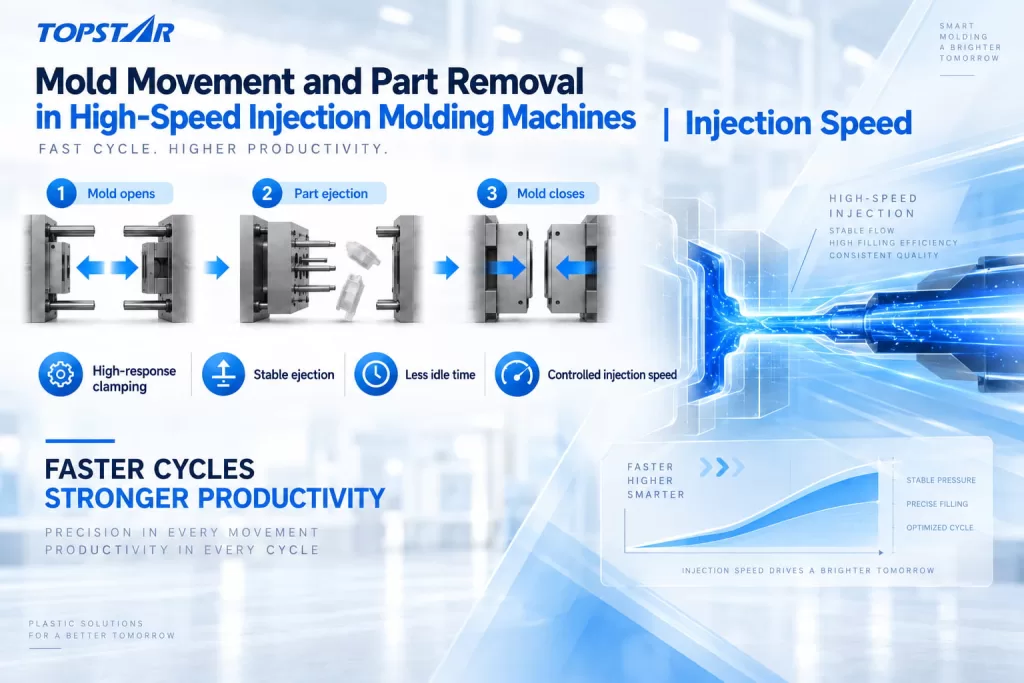
Mold Movement and Part Removal in High-Speed Injection Molding Machines, Injection Speed
Once the filling stage drops below one second, mold movement often becomes the key factor in shortening the molding cycle even further. Therefore, high-speed injection molding machines should minimize unnecessary time consumption in the following steps as much as possible:
Mold opening → Robot entry → Product removal → Robot exit → Mold closing
The mold opening stroke must be long enough to ensure reliable product removal while avoiding excessive length that would increase wasted motion. Similarly, the part-removal robot must have sufficient stroke and acceleration to remove all containers within the specified time, thereby avoiding becoming a new production bottleneck. When a mold has four, eight, or more cavities, it produces multiple containers at the same time, so the robot must remove every product within the limited mold-opening time. Even extremely fast injection speeds cannot offset efficiency losses from slow part removal or poor synchronization.
How Does Cooling Time Affect Container Warpage?
Cooling is the third key control factor, following mold movement and filling.
Thin-walled food containers cool relatively quickly due to their thin walls; however, they must still be rigid enough before the injection molding machine and removal system remove them from the mold. If manufacturers shorten the cooling time too much, the container’s sidewalls, edges, or bottom may develop issues due to temperature instability.
Common consequences include sidewall warpage, rim warpage, distortion, and stacking issues after demolding.
The reverse is also true. Once the container achieves sufficient rigidity, the marginal benefit of continued cooling in shortening the molding cycle diminishes. For high-volume packaging production lines, even an unnecessary delay of a few tenths of a second in mold closure can significantly affect total output.
Therefore, the most appropriate approach is:
Set the shortest possible cooling time while ensuring reliable demolding and stable handling in subsequent processes.
Cooling Time Should Only Be Reduced Once the Container Has Sufficient Rigidity
Cooling optimization should begin with the mold’s thermal state, rather than relying solely on the machine’s timing settings. Manufacturers should monitor the following parameters:
Mold cooling water temperature;
Water flow rate through the mold;
Cavity temperature distribution;
Product temperature at demolding;
Post-demolding deformation.
If shortening the cooling time increases container warpage, it indicates the process has exceeded the critical threshold for minimum safe rigidity. Before further reducing the cooling time, a better solution may be to improve the mold water circulation, rebalance the cooling channels, or reduce thermal resistance. For this reason, when adjusting a high-speed injection molding machine, it is necessary to optimize it as an integrated system comprising the mold and the cooling system.
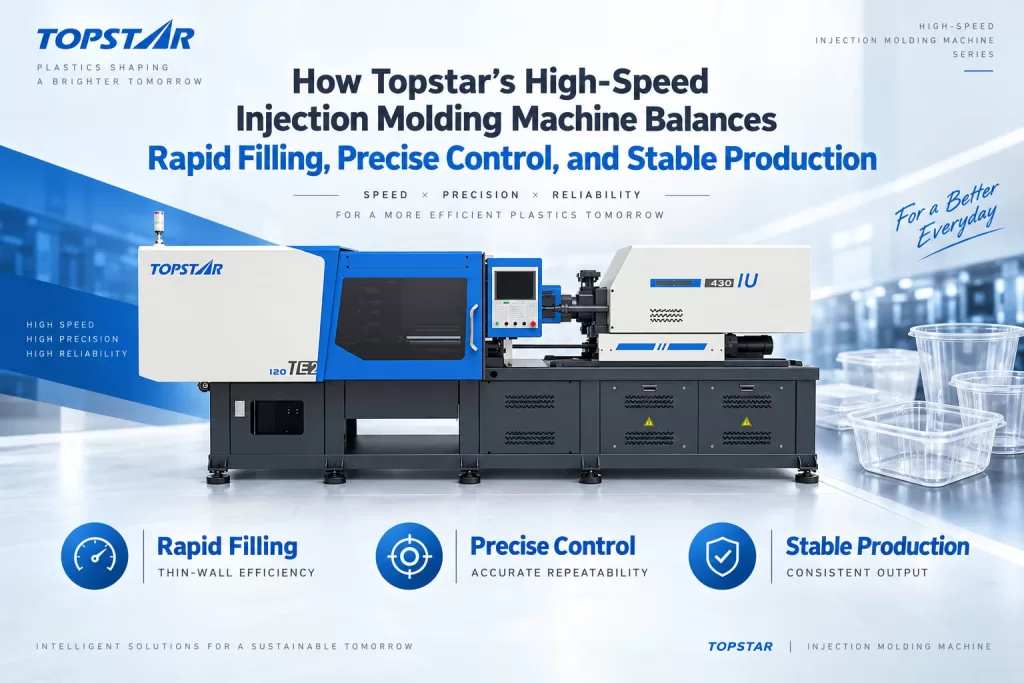
How Topstar’s High-Speed Injection Molding Machine Balance Rapid Filling, Precise Control, and Stable Production
Topstar’s TEII electric injection molding machines are designed to meet demanding applications that require high injection speed, precise repeatability, and consistent process stability.
The TEII series offers a maximum injection speed of up to 500 mm/s. Its high-speed servo drive system enables precise, coordinated control of position, speed, and pressure through rapid digital response. It offers injection repeatability of ±0.01 mm, and its integrated injection unit uses a high-rigidity structural design that minimizes deformation during injection.
For thin-walled food containers, this combined solution meets three key requirements during the molding cycle:
First, high-speed injection helps fill the cavity before the melt solidifies prematurely.
Second, precise servo control lets manufacturers reproduce specific injection molding profiles without operating at maximum speed throughout the entire filling phase.
Third, the high-rigidity clamping system and smooth mold movements help optimize the injection phase without sacrificing overall efficiency through slow mold opening, closing, or part removal.
Therefore, for thin-walled food containers, the most efficient molding cycle strategy can be summarized as follows:
Fill at a sufficiently fast speed to prevent premature solidification → Optimize mold opening and part removal → Adopt a solution that both prevents warpage and shortens cooling time → Achieve synchronized coordination throughout the entire molding cycle.
Shorter Molding Cycles for Thin-Walled Food Containers
For thin-walled food containers, short molding cycles are only possible when the entire production unit operates as a coordinated system.
The filling phase must be fast enough to prevent premature solidification of the melt; the cooling phase must stop immediately once the container reaches sufficient rigidity; and the mold opening and part removal phases must remove the finished containers quickly without causing warpage.
Topstar designed the TEII series electric injection molding machines to meet demanding high-speed production requirements. The machines deliver injection speeds of up to 500 mm/s and repeatability of ±0.01 mm, while their communication system responds in just 0.125 ms. A high-speed servo control system and highly rigid, low-friction mechanical structure further support fast, stable, and precise operation.
Therefore, for producing thin-walled food containers, the objective is not merely to increase injection speed, but to achieve the shortest, most stable production cycle by tightly coordinating filling, cooling, mold movement, and part removal.
TRENDING POSTS
- Breaking Through the Full Scene-to-AI Link! Topstar Industrial Data Collection Matrix Achieves Major Technical Breakthro 2026/09/23
- TOPSTAR Selected in “Forbes China AI Top 50” and Wins “2026 Embodied AI Industry Benchmark Award” 2026/09/23
- Topstar Achieves ISO 13849 Functional Safety Certification for Robotics 2026/09/23
- Topstar Completes Key Puzzle in Embodied Intelligence Data Closed Loop — Industrial AI Capability Foundation Now in Place 2026/09/23
HOT TOPIC
- .ervo motor-driven linear robots
- •
- 1.0 guangdong topstar technology co. ltd
- 1.0 topstar china
- 1.0 topstar robot
- 11
- 160℃ mold temperature controller
- 170 ton injection molding machine
- 2
- 21
- 220-ton injection molding machine
- 23
- 260 ton injection molding machine
- 3 axis robot
- 3 axis robots
- 3 in 1 Compact Dehumidifying Dryer
- 3-axis robot
- 3-axis robots
- 39
- 4 axis robot
- 4-axis SCARA robot
- 41
- 460T injection molding machine
- 5-axis CNC machine
- 62
- 90 ton injection molding machine
- accuracy
- Air Chillers
- air-cooled chillers
- all electric injection molding machine
- all electric injection molding machines
- all-electric injection molding machine
- All-electric injection molding machines
- and overall production quality. Therefore
- AP-RubberPlas
- auto cooling system
- auto loader
- Auto Loaders
- automated injection molding machine
- Automation changed engineering
- automation of injection molding robots
- automotive parts injection molding
- Auxiliary Equipment
- auxiliary machine
- Bench Injection Molding Machine
- cabinet dryer
- Cabinet dryer manufacturers
- Cabinet dryers
- cartesian coordinate robot
- Cartesian Coordinate Robots
- Cartesian injection robot
- Cartesian robot
- Central Feeding System
- Central Feeding Systems
- chiller
- CNC Drilling Machine
- CNC Drilling Machines
- cnc engraving machine manufacturer
- cnc laser cutting machine manufacturer
- CNC machine
- CNC Machine Center
- CNC Machine for Sale
- CNC Machine Manufacturing
- CNC Machine Tool
- CNC machine tool product
- CNC Machining Center
- CNC wood carving machine
- Compact Dehumidifying Dryer
- Cooling system
- Cross-Walking Single Axis Servo Cylinder Robot
- Cross-Walking Single-Axis Servo Cylinder Robot
- Cross-Walking Three-Axis/Five-Axis Servo Driven Robot
- cross-walking three-axis/five-axis servo-driven robot
- Dehumidifier Dryer
- Dehumidifying Dryer
- dehumidifying dryers
- delta parallel robot
- Desktop Injection Molding Machine
- Desktop injection molding machines
- Desktop Molding Machine
- desktop plastic injection machine
- Desktop Plastic Injection Molding Machine
- detachable autoloader
- Digital Transformation
- direct clamp injection molding machine
- Direct clamp injection molding machines
- Dosing & mixing system
- Drilling Centers
- Drying and dehumidification system
- drying and dehumidifying equipment
- Drying and Dehumidifying System
- drying system
- effective and efficient. Cabinet dryers are also used in other industries where large quantities of material need to be dried
- efficient injection molding machine
- elbow hydraulic injection molding machines
- electric injection molding machine
- electric injection molding machines
- energy-efficient injection molding robot
- energy-efficient water chiller
- energy-efficient water chillers
- energy-saving injection molding machine
- etc. Among injection molding robots
- exhibition
- features of CNC machine
- Feeding And Conveying System
- Five Axis Machine Center
- Flexible Production Line
- Fully automatic injection molding machine
- Gathering Topstar
- giant injection molding machine
- GMU-600 5-Axis Machining Center
- Granulating & Recycling System
- granulator machine
- gravimetric blender
- Heavy duty injection molding machine
- Heavy-Duty Take-Out Robot
- High-precision electric molding machines
- high-precision plastic molding machines
- high-speed all electric injection molding machine
- high-speed electric injection molding machine
- High-Speed Packaging Injection Molding
- Honeycomb rotor dehumidifier
- hopper dryer
- Hopper Dryers
- horizontal injection molding machine
- Horizontal Injection Molding Machines
- Horizontal Injection Moulding Machine
- Horizontal Mixer manufacturer
- How The CNC Machine Works
- hybrid injection molding machine
- hydraulic injection molding machine
- Hydraulic Injection Molding Machines
- in this article
- Industrial AI
- Industrial Automation
- Industrial robot
- Industrial Robot Chinese brand
- industrial robot parts
- industrial robot supplier
- Industrial robots
- Industry Chain
- Injection Manipulator
- injection manipulator robot
- injection mold machines
- Injection molding
- Injection molding automation
- Injection Molding Automation Solution
- injection molding dryer
- Injection molding equipment
- injection molding hopper dryer
- Injection molding machine
- injection molding machine brand
- Injection Molding Machine Factory
- Injection Molding Machine Manufacture
- Injection molding machine manufacturer
- injection molding machine manufacturers
- Injection molding machine procurement
- injection molding machine robotic arm
- injection molding machine with a robot
- Injection molding machines
- injection molding material dehumidifying
- injection molding plant
- injection molding process
- Injection Molding Robot
- injection molding robot arm
- Injection molding robot automation
- Injection molding robotic arm
- injection molding robots
- injection molding whole plant
- injection moulding dryer
- Injection moulding machine
- injection moulding machines
- Injection Moulding Robots
- Injection Robot
- Injection robot arm
- Injection robot manufacturer
- Injection robot wholesale
- injection robots
- Intelligent Factory
- intelligent injection molding machines
- Intelligent Manufacturing
- intelligent mold temperature
- intelligent mold temperature controller
- Intelligent mould temperature controller
- intelligent whole plant solution
- InterPlas Thailand 2025
- Introducing Injection Robot
- It is the best choice for drying large quantities of material at once. Cabinetmakers use these machines because they are fast
- Large flow water type mold temperature controller
- large injection molding machine
- large injection molding machines
- Learn what industrial automation and robotics is
- linear robot
- linear robots
- low speed sound-proof granulator
- machine plastic molding
- make sure to add some! Improvements (2) Keyphrase in introduction: Your keyphrase or its synonyms appear in the first paragraph of the copy
- manipulator machine
- manufacturing
- Manufacturing Innovation
- medical grade injection molding machines
- Medical Injection Molding
- medical injection molding machine
- medical injection molding machines
- micro injection molding machine
- middle speed granulator
- Mini CNC machine manufacturers.
- mobile cover making machine
- Mold Temperature Control System
- mold temperature controller
- mold temperature controllers
- molding machine
- molding material Dehumidifying System
- mould temperature control system
- mould temperature controller
- mould temperature controller
- mould temperature controllers
- New electric injection molding machine
- Nitrogen Dryer
- nitrogen dryer manufacturer
- nitrogen dryer system manufacturer
- Oil type mold temperature controller
- Oil type mold temperature controllers
- open day
- optical component injection molding
- Optical-grade dehumidifying dryer
- Outbound links: No outbound links appear in this page. Add some! Images: No images appear on this page. Add some! Internal links: No internal links appear in this page
- packaging injection molding
- Packaging Solutions
- PET Preform injection molding
- phone case maker machine
- phone case making machine
- phone cover making machine
- PID Control Mold Temperature Controller
- plastic auto loader
- plastic bottle making machine
- plastic bottle manufacturing
- plastic bucket making machine
- plastic bucket manufacturing
- Plastic chair making machine
- plastic dryer for injection molding
- plastic forming equipment
- Plastic Granulator
- Plastic Granulators
- plastic hopper dryer
- plastic injection machine
- plastic injection machines
- plastic injection molding
- Plastic injection molding equipment
- Plastic injection molding machine
- Plastic Injection Molding Machines
- plastic injection moulding machine
- plastic injection moulding machines
- plastic injection robot
- plastic molding
- Plastic Molding Industry
- Plastic Molding machine
- plastic molding machine 1
- Plastic Molding Machines
- plastic molding press
- plastic moulding machine
- plastic phone case making machine
- plastic-molding machine
- powerful granulator
- Powerful Type Sound-Proof Granulator
- precision injection molding
- precision injection molding machines
- production of plastic seats
- pure water mould temperature controller
- Robot injection molding
- robot injection molding machine
- robot manufacturing companies
- Robotic arm for injection molding machine
- robotic injection molding machines
- robotics in injection molding
- SCARA robot
- SCARA robots
- Screw dosers
- Service-oriented manufacturing
- Servo Cylinder Robot
- servo driven robot
- Servo Driven Robots
- servo injection molding machine
- servo injection robots
- servo motor-driven linear robots
- servo-driven 3-axis robot
- Servo-driven injection molding machine
- Servo-Driven Robot
- Setup of injection machine
- Silicone Injection Molding Machine
- six-axis industrial robot
- Smart Manufacturing
- soundproof granulator
- Sprue Picker
- Stainless Hopper Dryer
- Stainless Hopper Dryers
- star club
- swing arm robot
- T1 Cartesian injection robot
- take-out robot
- take-out robots
- Thailand 4.0
- the choice between servo-driven robots and hydraulic robots will have a certain impact on efficiency
- the most popular injection molding machine
- the type of injection molding robot
- TIC2000 Control System
- TMII injection molding machine
- toggle clamp injection molding machine
- Toggle Hydraulic Injection Molding Machines
- toggle injection molding machine
- Top 10 brands of injection robots
- Topstar
- Topstar Electric Injection Molding Machine InterPlas Thailand 2025 Smart Manufacturing Thailand 4.0
- Topstar Engineering
- Topstar Industrial Robots
- Topstar injection molding intelligent
- Topstar Scara Robots
- Useful Injection molding machine
- Vertical machining centers
- volumetric type blender
- Washing Machine Case Molding Solution
- water chiller
- water chillers
- water distributor
- water type mold temperature controller
- Water Type MoldTemperature Controller
- Water-Cooled Chillers
- Water-cooled Mold Temperature Controller
- water-type mold temperature controller
- Water-Type Mould Temperature Controllers
- We often face choices when performing injection molding. We will choose the type of injection molding machine
- wholesale of injection molding machines
- x carve CNC
- 热门查询 点击次数 展示 排名 topstar