How Does Topstar Support Filling Balance and Uniform Wall Thickness in Thin-Wall Packaging Products?
2026/11/20 By le zhan
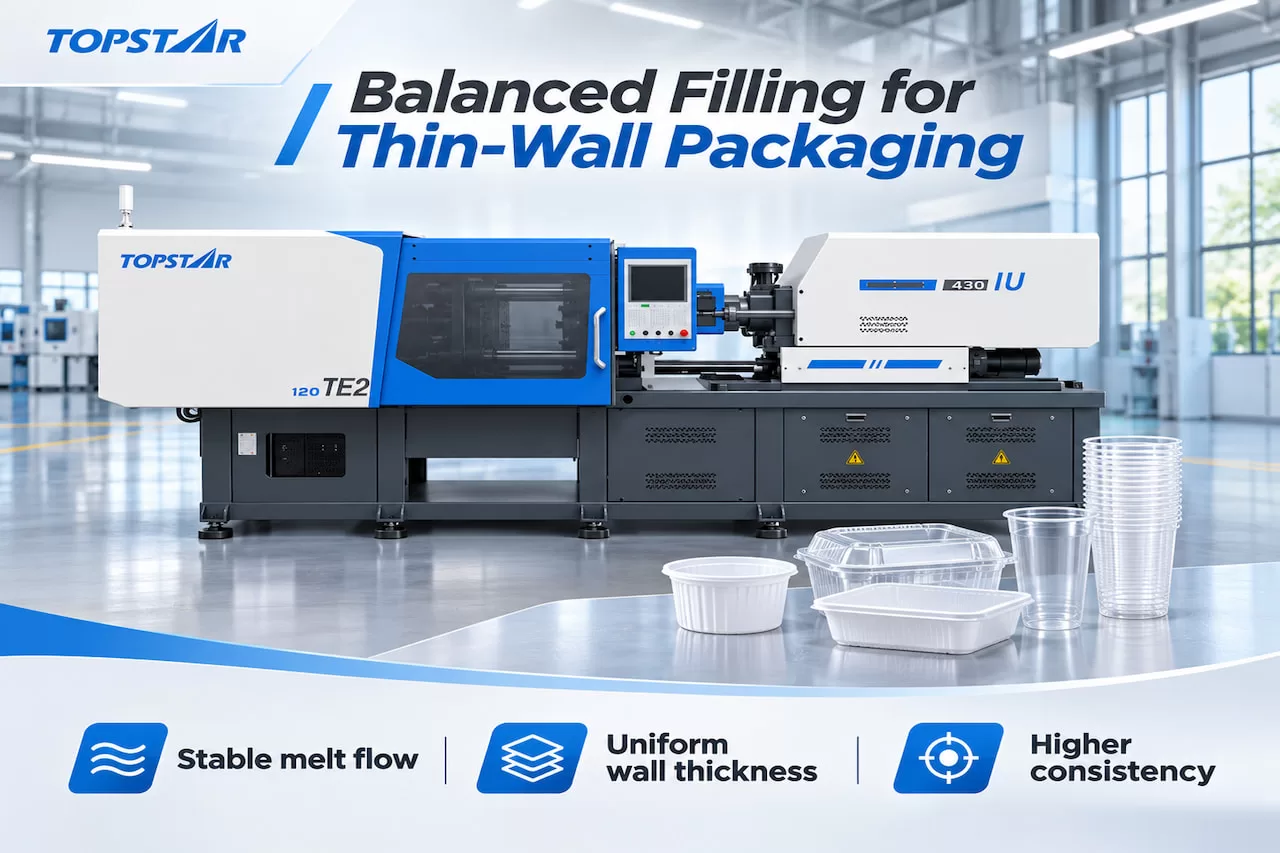
In producing thin-walled packaging products, the challenge lies not only in ensuring that molten plastic fills the mold cavity before it cools. The melt must also reach all areas of the cavity at a uniform rate to avoid localized overfilling or underfilling. Therefore, injection speed, pressure control, and mold stability are critical to achieving uniform wall thickness. To address the challenges of injection molding in the thin-wall packaging industry, Topstar’s TEII series electric injection molding machines offers a variety of injection unit configurations and features a highly rigid machine frame, effectively supporting a stable thin-wall injection molding process.
Why Is It Difficult to Achieve Balanced Filling and Consistent Wall Thickness in Thin-Wall Packaging Products?
Producing thin-wall packaging products places higher demands on the injection molding process, as the melt must flow through narrow cavity areas within a limited time. However, rapid cavity filling does not necessarily guarantee part uniformity. Variations in flow resistance, cooling conditions, runner geometry, and mold support structures can all lead to uneven filling, which in turn causes inconsistent wall thickness.
Why Do Thin-Wall Packaging Products Require a Faster and More Controllable Filling Process?
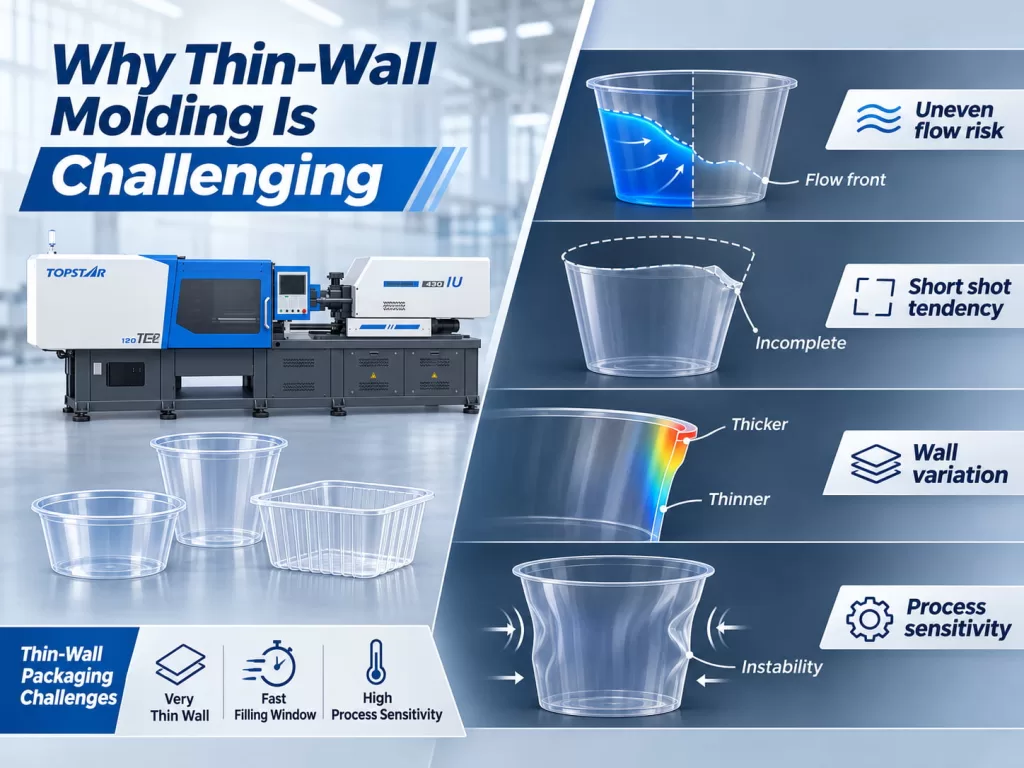
Thin-wall packaging products (such as disposable food containers, cups, and trays) typically have a high surface area-to-wall thickness ratio. This high flow length-to-wall thickness ratio makes it difficult for the molten plastic to reach the far end of the cavity before it cools.
When the melt comes into contact with the mold surface, it loses heat, increasing viscosity. If the injection speed is insufficient or unstable, the flow front may cool prematurely, leading to problems such as short shots, incomplete filling, or inconsistent wall thickness. Multi-cavity molds also present additional challenges. Because runner length, gate size, and cavity resistance vary, filling rates may differ between cavities even if the injection molding machine maintains a constant overall injection speed.
Therefore, the injection molding of thin-walled packaging products requires a well-designed injection speed profile and stable melt delivery. The goal is to ensure uniform filling of each cavity while avoiding excessive shear forces, flash, or other molding defects.
What Causes Uneven Wall Thickness During Injection Molding?
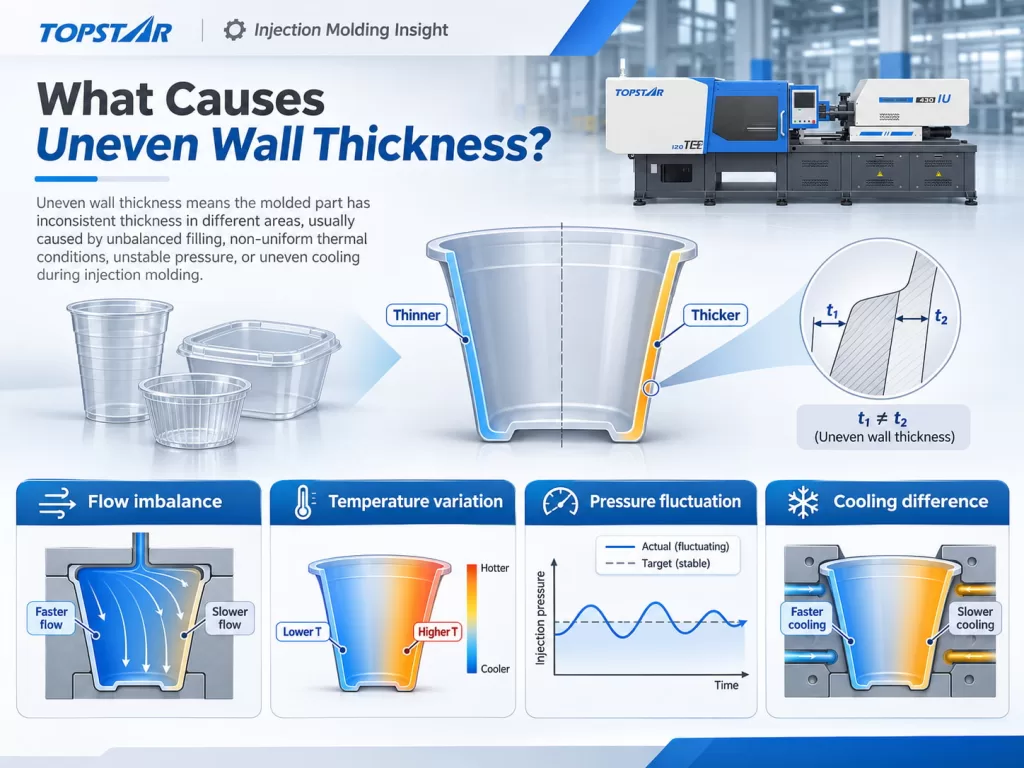
Wall thickness variations are not determined solely by injection speed but result from the combined effects of multiple factors, including mold design, injection pressure, temperature distribution, and machine configuration.
Among these, the following three factors require particular attention:
- Gate and runner design: Inconsistent flow resistance can lead to differences in filling rates between different areas or cavities, resulting in uneven material distribution.
- Injection Pressure and Hold Pressure: If the “speed-pressure” (V/P) switch point is set improperly, or if the hold pressure is unstable, it will affect the filling density within the cavity, the shrinkage rate, and the final product dimensions.
- Mold Temperature and Structural Support: Uneven cooling can lead to variations in shrinkage rates; meanwhile, insufficient platen rigidity or uneven mold support may affect mold alignment accuracy and product dimensional consistency.
If one cavity fills earlier than the others, the pressure and cooling processes experienced by the melt within that cavity will also differ. Increasing the overall injection speed may improve the situation for cavities that fill more slowly. However, it may also cause flash or overfilling (excessive holding pressure) in cavities that fill more quickly.
For this reason, when evaluating injection molding performance, it is essential to comprehensively consider mold balance, cooling channel layout, clamping conditions, and actual wall thickness measurements.
How Does Topstar Improve Filling Stability and Wall Thickness Consistency in Thin-Wall Packaging Products?
Once the molding challenges are identified, equipment selection becomes much clearer. Topstar’s TEII electric injection molding machine addresses the demands of thin-wall production through three complementary dimensions: injection unit configuration, precise control of injection motion and pressure, and robust mold support. These features enable manufacturers to match machine performance to varying wall-thickness requirements while keeping molding conditions highly consistent. Of course, the final molding result still depends on whether the mold, resin material, and process parameters are within the appropriate operating range.
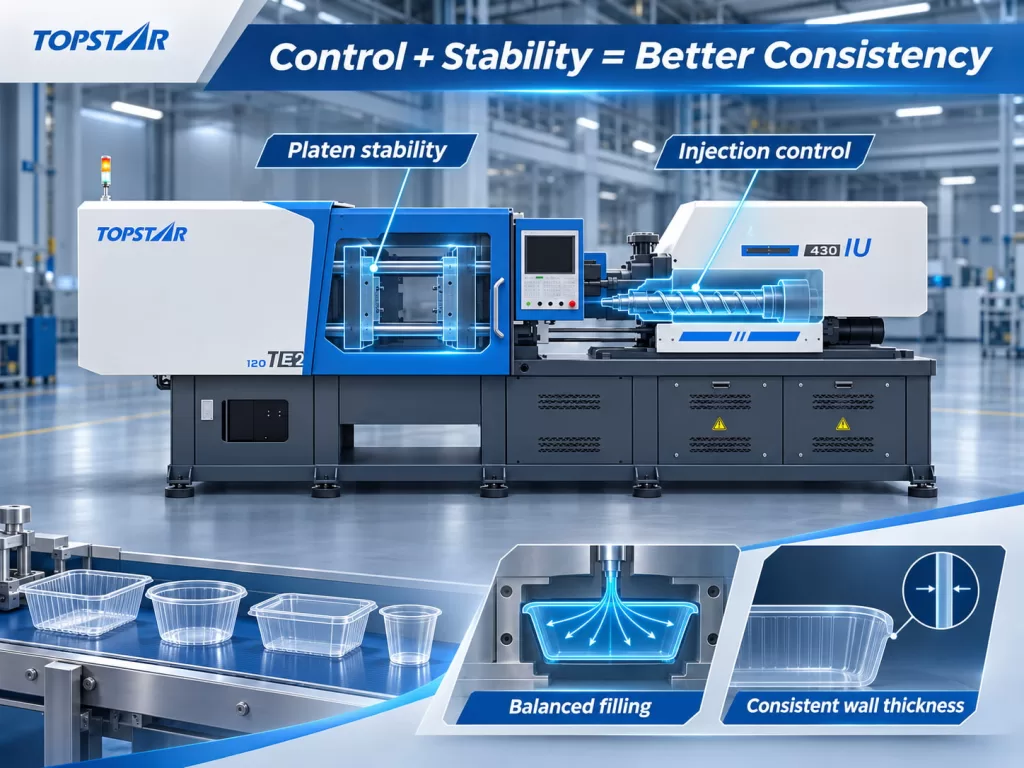
How Do the IU-h and IU-hs Injection Units Adapt to Different Filling Requirements?
The TEII electric injection molding machine offers three injection unit configurations to meet the production needs of different products:
| Injection Unit | Injection Characteristics | Application |
|---|---|---|
| IU | Normal speed, extended holding pressure | Thick-wall products |
| IU-h | Medium-speed injection | Thin-wall products |
| IU-hs | High-speed injection | Ultra-thin-wall products |
The IU-h is suitable for standard thin-wall products, with its “medium-speed” injection capability sufficient to meet filling requirements. For products that do not require extremely high injection speeds, it achieves a good balance between filling speed and process control.
The IU-hs, on the other hand, is designed for “ultra-thin-wall” applications, ensuring the melt fills narrow cavities in a very short time. Its high-speed injection capability effectively reduces the risk of premature melt cooling and incomplete filling.
Additionally, when selecting a model, we recommend comprehensively considering factors such as product wall thickness, flow length, resin viscosity, gate size, runner design, and required filling time.
These three configurations correspond to “normal-speed,” “medium-speed,” and “high-speed” injection characteristics, respectively, thereby meeting the production requirements for thick-walled, thin-walled, and ultra-thin-walled products. (Topstar TEII Series Product Brochure)
How Can Injection Control and Platen Stability Improve Consistency?
Selecting the appropriate injection unit is only the first step. Ensuring consistent wall thickness also depends on the machine’s ability to control the injection process and maintain precise mold stability.
The TEII electric injection molding machine features an integrated injection structure and optional linear guide support. Its low-damping design reduces mechanical resistance and improves motion sensitivity, enabling more precise injection control and pressure feedback. When equipped with linear guides, the TEII series can achieve low-speed control below 1 mm/s, with injection repeatability as high as ±0.01 mm and platen parallelism error below 0.05 mm. While these machine parameters contribute to process stability, high-rigidity platens and an optimized mold support design ensure the mold remains consistently aligned throughout repeated production cycles.
How to Verify Filling Balance and Wall Thickness Consistency?
Selecting the appropriate injection unit and machine configuration lays the foundation for producing thin-walled products, but the final results must still be verified through actual trial runs. Engineers should evaluate part weight, wall thickness at various locations, cavity-filling balance, and dimensional consistency across multiple production cycles. Subsequently, injection speed, V/P switch points, holding pressure, and mold temperature can be adjusted based on the measurement results.
Ultimately, achieving filling balance and uniform wall thickness requires the coordinated interaction of the injection unit, the injection control system, and the mold support structure. The Topstar TEII electric injection molding machine offers two configurations—IU-h and IU-hs—to accommodate different thin-wall application requirements, ensuring more stable and repeatable quality for thin-wall packaging products.
TRENDING POSTS
- TOPS DAY 2026: Turning Industrial AI into Real-World Impact 2026/11/20
- Breaking Through the Full Scene-to-AI Link! Topstar Industrial Data Collection Matrix Achieves Major Technical Breakthro 2026/11/20
- TOPSTAR Selected in “Forbes China AI Top 50” and Wins “2026 Embodied AI Industry Benchmark Award” 2026/11/20
- Topstar Achieves ISO 13849 Functional Safety Certification for Robotics 2026/11/20
HOT TOPIC
- .ervo motor-driven linear robots
- •
- 1.0 guangdong topstar technology co. ltd
- 1.0 topstar china
- 1.0 topstar robot
- 11
- 160℃ mold temperature controller
- 170 ton injection molding machine
- 2
- 21
- 220-ton injection molding machine
- 23
- 260 ton injection molding machine
- 3 axis robot
- 3 axis robots
- 3 in 1 Compact Dehumidifying Dryer
- 3-axis robot
- 3-axis robots
- 39
- 4 axis robot
- 4-axis SCARA robot
- 41
- 460T injection molding machine
- 5-axis CNC machine
- 62
- 90 ton injection molding machine
- accuracy
- Air Chillers
- air-cooled chillers
- all electric injection molding machine
- all electric injection molding machines
- all-electric injection molding machine
- All-electric injection molding machines
- and overall production quality. Therefore
- AP-RubberPlas
- auto cooling system
- auto loader
- Auto Loaders
- automated injection molding machine
- Automation changed engineering
- automation of injection molding robots
- automotive parts injection molding
- Auxiliary Equipment
- auxiliary machine
- Bench Injection Molding Machine
- cabinet dryer
- Cabinet dryer manufacturers
- Cabinet dryers
- cartesian coordinate robot
- Cartesian Coordinate Robots
- Cartesian injection robot
- Cartesian robot
- Central Feeding System
- Central Feeding Systems
- chiller
- CNC Drilling Machine
- CNC Drilling Machines
- cnc engraving machine manufacturer
- cnc laser cutting machine manufacturer
- CNC machine
- CNC Machine Center
- CNC Machine for Sale
- CNC Machine Manufacturing
- CNC Machine Tool
- CNC machine tool product
- CNC Machining Center
- CNC wood carving machine
- Compact Dehumidifying Dryer
- Cooling system
- Cross-Walking Single Axis Servo Cylinder Robot
- Cross-Walking Single-Axis Servo Cylinder Robot
- Cross-Walking Three-Axis/Five-Axis Servo Driven Robot
- cross-walking three-axis/five-axis servo-driven robot
- Dehumidifier Dryer
- Dehumidifying Dryer
- dehumidifying dryers
- delta parallel robot
- Desktop Injection Molding Machine
- Desktop injection molding machines
- Desktop Molding Machine
- desktop plastic injection machine
- Desktop Plastic Injection Molding Machine
- detachable autoloader
- Digital Transformation
- direct clamp injection molding machine
- Direct clamp injection molding machines
- Dosing & mixing system
- Drilling Centers
- Drying and dehumidification system
- drying and dehumidifying equipment
- Drying and Dehumidifying System
- drying system
- effective and efficient. Cabinet dryers are also used in other industries where large quantities of material need to be dried
- efficient injection molding machine
- elbow hydraulic injection molding machines
- electric injection molding machine
- electric injection molding machines
- energy-efficient injection molding robot
- energy-efficient water chiller
- energy-efficient water chillers
- energy-saving injection molding machine
- etc. Among injection molding robots
- exhibition
- features of CNC machine
- Feeding And Conveying System
- Five Axis Machine Center
- Flexible Production Line
- Fully automatic injection molding machine
- Gathering Topstar
- giant injection molding machine
- GMU-600 5-Axis Machining Center
- Granulating & Recycling System
- granulator machine
- gravimetric blender
- Heavy duty injection molding machine
- Heavy-Duty Take-Out Robot
- High-precision electric molding machines
- high-precision plastic molding machines
- high-speed all electric injection molding machine
- high-speed electric injection molding machine
- High-Speed Packaging Injection Molding
- Honeycomb rotor dehumidifier
- hopper dryer
- Hopper Dryers
- horizontal injection molding machine
- Horizontal Injection Molding Machines
- Horizontal Injection Moulding Machine
- Horizontal Mixer manufacturer
- How The CNC Machine Works
- hybrid injection molding machine
- hydraulic injection molding machine
- Hydraulic Injection Molding Machines
- in this article
- Industrial AI
- Industrial Automation
- Industrial robot
- Industrial Robot Chinese brand
- industrial robot parts
- industrial robot supplier
- Industrial robots
- Industry Chain
- Injection Manipulator
- injection manipulator robot
- injection mold machines
- Injection molding
- Injection molding automation
- Injection Molding Automation Solution
- injection molding dryer
- Injection molding equipment
- injection molding hopper dryer
- Injection molding machine
- injection molding machine brand
- Injection Molding Machine Factory
- Injection Molding Machine Manufacture
- Injection molding machine manufacturer
- injection molding machine manufacturers
- Injection molding machine procurement
- injection molding machine robotic arm
- injection molding machine with a robot
- Injection molding machines
- injection molding material dehumidifying
- injection molding plant
- injection molding process
- Injection Molding Robot
- injection molding robot arm
- Injection molding robot automation
- Injection molding robotic arm
- injection molding robots
- injection molding whole plant
- injection moulding dryer
- Injection moulding machine
- injection moulding machines
- Injection Moulding Robots
- Injection Robot
- Injection robot arm
- Injection robot manufacturer
- Injection robot wholesale
- injection robots
- Intelligent Factory
- intelligent injection molding machines
- Intelligent Manufacturing
- intelligent mold temperature
- intelligent mold temperature controller
- Intelligent mould temperature controller
- intelligent whole plant solution
- InterPlas Thailand 2025
- Introducing Injection Robot
- It is the best choice for drying large quantities of material at once. Cabinetmakers use these machines because they are fast
- Large flow water type mold temperature controller
- large injection molding machine
- large injection molding machines
- Learn what industrial automation and robotics is
- linear robot
- linear robots
- low speed sound-proof granulator
- machine plastic molding
- make sure to add some! Improvements (2) Keyphrase in introduction: Your keyphrase or its synonyms appear in the first paragraph of the copy
- manipulator machine
- manufacturing
- Manufacturing Innovation
- medical grade injection molding machines
- Medical Injection Molding
- medical injection molding machine
- medical injection molding machines
- micro injection molding machine
- middle speed granulator
- Mini CNC machine manufacturers.
- mobile cover making machine
- Mold Temperature Control System
- mold temperature controller
- mold temperature controllers
- molding machine
- molding material Dehumidifying System
- mould temperature control system
- mould temperature controller
- mould temperature controller
- mould temperature controllers
- New electric injection molding machine
- Nitrogen Dryer
- nitrogen dryer manufacturer
- nitrogen dryer system manufacturer
- Oil type mold temperature controller
- Oil type mold temperature controllers
- open day
- optical component injection molding
- Optical-grade dehumidifying dryer
- Outbound links: No outbound links appear in this page. Add some! Images: No images appear on this page. Add some! Internal links: No internal links appear in this page
- packaging injection molding
- Packaging Solutions
- PET Preform injection molding
- phone case maker machine
- phone case making machine
- phone cover making machine
- PID Control Mold Temperature Controller
- plastic auto loader
- plastic bottle making machine
- plastic bottle manufacturing
- plastic bucket making machine
- plastic bucket manufacturing
- Plastic chair making machine
- plastic dryer for injection molding
- plastic forming equipment
- Plastic Granulator
- Plastic Granulators
- plastic hopper dryer
- plastic injection machine
- plastic injection machines
- plastic injection molding
- Plastic injection molding equipment
- Plastic injection molding machine
- Plastic Injection Molding Machines
- plastic injection moulding machine
- plastic injection moulding machines
- plastic injection robot
- plastic molding
- Plastic Molding Industry
- Plastic Molding machine
- plastic molding machine 1
- Plastic Molding Machines
- plastic molding press
- plastic moulding machine
- plastic phone case making machine
- plastic-molding machine
- powerful granulator
- Powerful Type Sound-Proof Granulator
- precision injection molding
- precision injection molding machines
- production of plastic seats
- pure water mould temperature controller
- Robot injection molding
- robot injection molding machine
- robot manufacturing companies
- Robotic arm for injection molding machine
- robotic injection molding machines
- robotics in injection molding
- SCARA robot
- SCARA robots
- Screw dosers
- Service-oriented manufacturing
- Servo Cylinder Robot
- servo driven robot
- Servo Driven Robots
- servo injection molding machine
- servo injection robots
- servo motor-driven linear robots
- servo-driven 3-axis robot
- Servo-driven injection molding machine
- Servo-Driven Robot
- Setup of injection machine
- Silicone Injection Molding Machine
- six-axis industrial robot
- Smart Manufacturing
- soundproof granulator
- Sprue Picker
- Stainless Hopper Dryer
- Stainless Hopper Dryers
- star club
- swing arm robot
- T1 Cartesian injection robot
- take-out robot
- take-out robots
- Thailand 4.0
- the choice between servo-driven robots and hydraulic robots will have a certain impact on efficiency
- the most popular injection molding machine
- the type of injection molding robot
- TIC2000 Control System
- TMII injection molding machine
- toggle clamp injection molding machine
- Toggle Hydraulic Injection Molding Machines
- toggle injection molding machine
- Top 10 brands of injection robots
- Topstar
- Topstar Electric Injection Molding Machine InterPlas Thailand 2025 Smart Manufacturing Thailand 4.0
- Topstar Engineering
- Topstar Industrial Robots
- Topstar injection molding intelligent
- Topstar Scara Robots
- Useful Injection molding machine
- Vertical machining centers
- volumetric type blender
- Washing Machine Case Molding Solution
- water chiller
- water chillers
- water distributor
- water type mold temperature controller
- Water Type MoldTemperature Controller
- Water-Cooled Chillers
- Water-cooled Mold Temperature Controller
- water-type mold temperature controller
- Water-Type Mould Temperature Controllers
- We often face choices when performing injection molding. We will choose the type of injection molding machine
- wholesale of injection molding machines
- x carve CNC
- 热门查询 点击次数 展示 排名 topstar